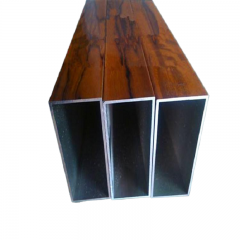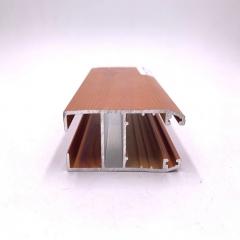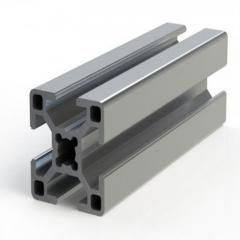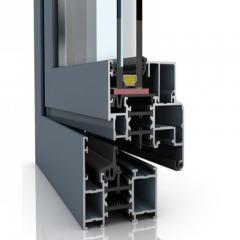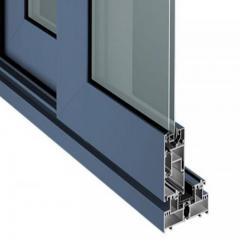
What is an aluminum extrusion? At its core, it's a manufacturing process that forces heated aluminum through a shaped die to create profiles with consistent cross-sections. But here's what many engineers overlook: the specific aluminum composition you choose fundamentally determines whether your project succeeds or fails. Aluminum extrusion alloys are precisely engineered metal compositions designed specifically for this extrusion process, combining base aluminum with carefully measured amounts of elements like magnesium, silicon, copper, and zinc to achieve targeted mechanical properties.
Think of it this way—pure aluminum is soft and lacks the structural strength most applications demand. By strategically adding alloying elements, manufacturers can create materials that are stronger, more corrosion-resistant, or easier to form into complex shapes. This is the aluminum extrusion definition in practice: transforming a versatile base metal into specialized materials tailored for specific performance requirements.
Choosing the wrong alloy can derail an entire project. You might end up paying premium prices for strength you don't need, or worse, discover your extruded aluminum profiles crack during welding or fail prematurely in harsh environments. The right selection, however, delivers the opposite outcome.
Selecting the optimal aluminum extrusion alloy can simultaneously reduce material costs by 15-30% while improving performance—a rare win-win that comes from matching alloy capabilities precisely to application requirements.
This comprehensive guide serves as your single-source reference for understanding aluminum alloys used in extrusion. Rather than piecing together scattered information from multiple websites, you'll find everything you need here—from alloy series breakdowns and mechanical property comparisons to temper designations and industry-specific recommendations.
To define extruded aluminum properly, you need to understand what happens at the molecular level. When alloying elements are added to aluminum, they integrate into the crystal lattice structure, fundamentally changing how the metal behaves. Each element contributes specific characteristics:
These elements don't just add to aluminum's properties—they transform them. For example, when you combine magnesium and silicon in the 6xxx series alloys, you create a material that responds exceptionally well to heat treatment, achieving strength levels far exceeding what either element alone could provide.
Throughout this guide, you'll discover exactly how to evaluate alloy properties, understand temper designations, assess extrudability ratings, and match surface finishing requirements to your specific application. Whether you're designing architectural facades, automotive components, or aerospace structures, the principles you'll learn here will help you make informed decisions that balance performance, cost, and manufacturability.
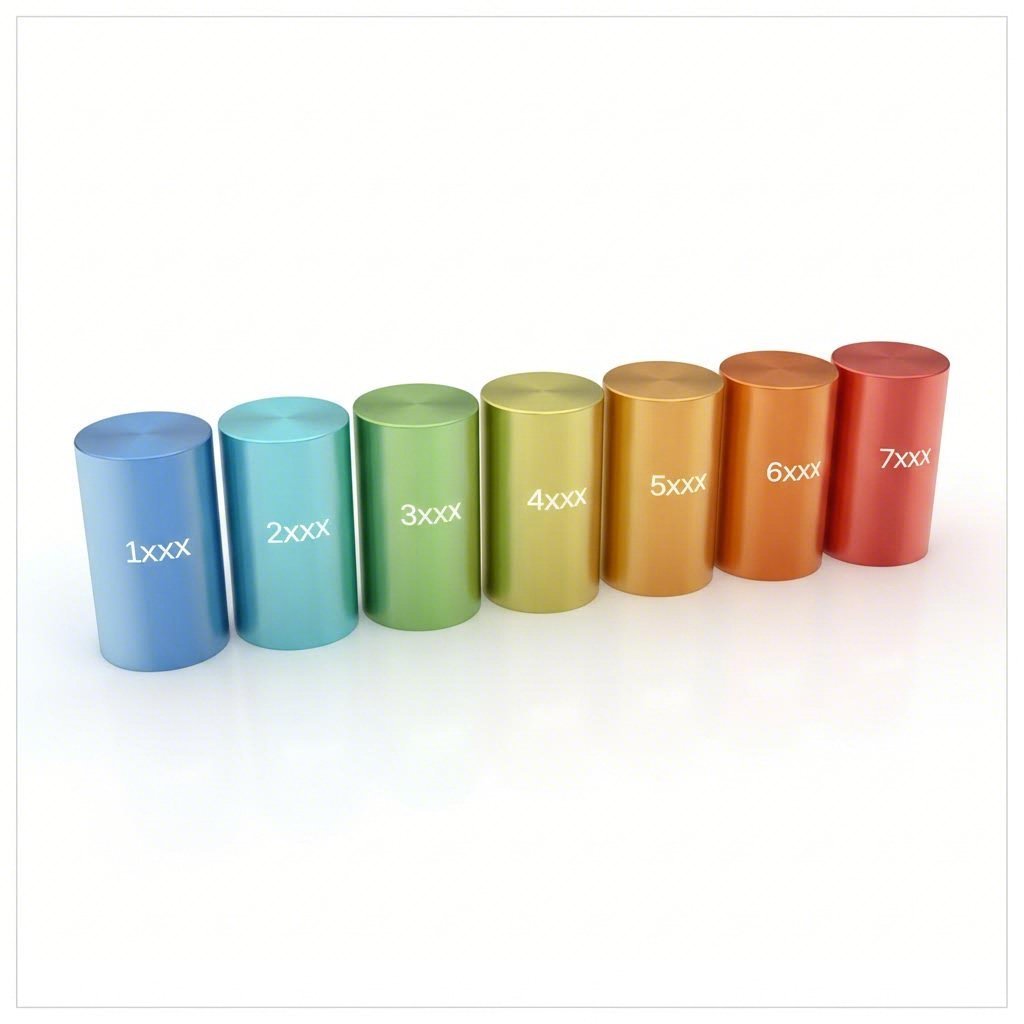
Ever looked at an aluminum specification like "6061-T6" and wondered what those numbers actually mean? You're not alone. The aluminum alloy designation system might seem cryptic at first, but once you understand the logic behind it, selecting the right material becomes significantly easier. Let's decode this numbering system so you can confidently navigate the aluminum alloys list and identify exactly what you need.
Wrought aluminum alloys use a four-digit numbering system that tells you everything essential about the material's composition. Here's how to read it:
For example, according to United Aluminum, in Alloy 5183, the "5" indicates magnesium is the principal alloying element, the "1" tells you it's the first modification of the original 5083 alloy, and "83" indicates the sequence in which this alloy was created within the 5xxx series.
This systematic approach makes it straightforward to compare common alloys of aluminum and quickly understand their fundamental characteristics just by glancing at the designation.
Each aluminum series offers distinct properties that make it suitable—or unsuitable—for extrusion applications. Understanding these differences is crucial when evaluating types of aluminum alloys for your project. The table below consolidates all seven series into a single reference, highlighting what matters most for extrusion applications:
| Series | Primary Alloying Elements | Key Characteristics | Extrudability Rating | Primary Applications |
|---|---|---|---|---|
| 1xxx | 99%+ Pure Aluminum | High corrosion resistance, excellent workability, good finishing, not heat-treatable | Excellent | Chemical equipment, food handling, liquid containers, electrical conductors |
| 2xxx | Copper | High mechanical strength, superior machinability, heat-treatable, requires corrosion protection | Poor | Aerospace structures, high-strength applications, military components |
| 3xxx | Manganese | Moderate strength, good corrosion resistance, highly ductile, great for forming, not heat-treatable | Good | Heat exchangers, condensers, cooking utensils, chemical storage |
| 4xxx | Silicon | Lower melting point, good wear resistance, not satisfying extrudability properties | Limited | Welding wire and filler materials, forged components |
| 5xxx | Magnesium | High marine corrosion resistance, excellent weldability, moderate strength, not heat-treatable | Moderate to Good | Marine applications, pressure vessels, automotive panels, architectural trim |
| 6xxx | Magnesium + Silicon | Balanced strength, excellent formability, superb weldability, heat-treatable, corrosion resistant | Excellent | Architectural profiles, structural components, automotive, general engineering |
| 7xxx | Zinc | Very high tensile strength, heat-treatable, good machinability, not suitable for bending | Poor to Moderate | Aerospace frames, high-performance sports equipment, military applications |
As you can see from this al alloy grades comparison, extrudability varies dramatically across series. This directly impacts what shapes you can create, how complex your profiles can be, and ultimately, your production costs.
Among all common aluminium alloys, the 6xxx series stands out as the undisputed champion for extrusion applications. What makes these alloys so special? The combination of magnesium and silicon creates several advantages:
Popular aluminum material types within this series include 6063 for architectural applications requiring fine finishes, 6061 for structural applications demanding higher strength, and 6005 and 6082 for applications needing a balance between the two.
When strength-to-weight ratio becomes the critical factor—think aerospace and defense applications—the 7xxx series enters the picture. These zinc-alloyed materials deliver tensile strength levels that rival many steel alloys while maintaining aluminum's weight advantage.
However, this strength comes with tradeoffs. The 7xxx series presents significant extrusion challenges, limiting profile complexity and increasing production costs. These alloys also lack the formability of other aluminum series, making them unsuitable for applications requiring post-extrusion bending.
Understanding these aluminum series characteristics gives you the foundation needed to narrow down your alloy selection. But within each series, individual alloys offer distinct performance profiles that can make or break your application.
Now that you understand the aluminum alloy series system, let's zoom in on the workhorses of the extrusion industry. When engineers specify extruded aluminum profiles, four alloys dominate the conversation: 6063, 6061, 6005, and 6082. Each brings distinct advantages to the table, and understanding their differences can mean the difference between a project that exceeds expectations and one that falls short.
What makes these alloys different from each other when they're all part of the same 6xxx family? The answer lies in subtle but significant variations in their chemical composition—small changes in magnesium, silicon, and trace elements that dramatically alter performance characteristics.
These two alloys represent the most common aluminum grades in the extrusion world, yet they serve fundamentally different purposes. Think of 6063 as the "architectural aluminum" and 6061 as the "structural aluminum." This distinction stems directly from their chemical makeup.
According to Industrial Metal Service, 6061 aluminum contains 0.15-0.4% copper and 0.8-1.2% magnesium, while 6063 limits copper to just 0.10% maximum and magnesium to 0.45-0.90%. These seemingly small differences create substantial performance gaps.
Here's a detailed comparison of mechanical properties across common tempers:
| Property | 6061-T4 | 6061-T6 | 6063-T4 | 6063-T6 |
|---|---|---|---|---|
| Tensile Strength | 35,000 psi | 45,000 psi | 25,000 psi | 35,000 psi |
| Yield Strength | 21,000 psi | 40,000 psi | 13,000 psi | 31,000 psi |
| Shear Strength | 24,000 psi | 30,000 psi | 16,000 psi | 22,000 psi |
| Brinell Hardness | 65 | 95 | 46 | 73 |
| Modulus of Elasticity | 10,000 ksi | 10,000 ksi | 10,000 ksi | 10,000 ksi |
Notice something interesting? Untempered 6061-T4 actually matches or exceeds the strength of heat-treated 6063-T6 in most categories. This makes 6061 the clear choice when structural integrity matters most.
So why would anyone choose 6063 aluminum extrusion? The answer becomes clear when you consider surface quality. The lower copper content in 6063 produces a purer aluminum matrix that responds beautifully to anodizing and other finishing processes. This is why window frames, door frames, and decorative architectural elements almost universally use 6063.
Here's something many specifications overlook: welding significantly reduces the strength of heat-treated aluminum extrusion alloys. When you weld 6063-T6, you can expect approximately a 30% reduction in strength in the heat-affected zone. The material essentially reverts to a condition closer to T4 temper in those areas.
This same principle applies to 6061, though its higher base strength means it often retains adequate performance even after welding. If your application requires welded assemblies under load, factor this strength reduction into your design calculations or consider post-weld heat treatment to restore properties.
Both alloys weld readily using standard techniques, but 6061 offers slightly better weldability due to its higher silicon content, which improves fluidity during fusion. For applications like bicycle frames, automotive parts, or structural welded assemblies, this advantage can influence alloy selection.
What if you need something between 6063's excellent extrudability and 6061's superior strength? That's precisely where 6005 and 6082 enter the picture. These aluminium alloy extrusion options offer compelling middle-ground solutions.
According to MakeItFrom.com, both alloys share 99% of their composition in common, yet subtle differences create distinct performance profiles:
| Property | 6005 | 6082 |
|---|---|---|
| Tensile Strength (UTS) | 190-310 MPa | 140-340 MPa |
| Yield Strength | 100-280 MPa | 85-320 MPa |
| Elongation at Break | 9.5-17% | 6.3-18% |
| Brinell Hardness | 90-95 | 40-95 |
| Thermal Conductivity | 180-200 W/m-K | 160 W/m-K |
| Fatigue Strength | 55-95 MPa | 55-130 MPa |
| Magnesium Content | 0.4-0.6% | 0.6-1.2% |
| Manganese Content | 0-0.1% | 0.4-1.0% |
The key differentiator? Manganese content. 6082 contains significantly more manganese (0.4-1.0% versus 0-0.1%), which contributes to its higher potential strength and improved fatigue resistance. This makes 6082 a popular choice in European markets for structural applications, transportation equipment, and offshore structures.
6005, on the other hand, offers better thermal conductivity and more consistent hardness values. It's often specified for heat exchangers, ladder components, and applications where predictable mechanical properties matter more than peak strength.
While 6xxx alloys handle most extrusion applications, some projects demand strength levels these alloys simply cannot deliver. This is where 7075 extrusion enters the conversation. With zinc as its primary alloying element, 7075 achieves tensile strength approaching 83,000 psi—nearly double that of 6061-T6.
However, this extruded aluminum alloy comes with significant tradeoffs. Its poor extrudability limits profile complexity, and its reduced corrosion resistance often requires protective coatings. For aerospace components, high-performance sporting goods, and military applications where strength-to-weight ratio trumps all other considerations, the tradeoffs are worthwhile. For most commercial applications, the 6xxx series remains the practical choice.
Understanding these mechanical properties and composition differences empowers you to specify the right alloy from the start. But raw alloy selection is only part of the equation—the temper designation you choose transforms these base materials into finished products with precisely tuned performance characteristics.
You've selected the perfect alloy for your project—but you're only halfway there. That letter and number combination following the alloy designation? It's not just industry jargon. The aluminum temper you specify determines whether your extrusion arrives soft and formable or hardened and ready for structural duty. Understanding how aluminum extrusion processing affects final properties separates successful projects from costly redesigns.
When you see a specification like "6061-T6," the "T6" tells you exactly how that material was treated after extrusion. This temper designation, standardized under ANSI H35.1, communicates critical information about strength, formability, and performance characteristics. Let's decode what these designations mean for your application.
The aluminum temper system uses letters to indicate basic treatment categories, by numbers that specify exact processing conditions. For extruded aluminum, the "T" designation dominates—indicating the material has been heat-treated to produce stable tempers other than F (as-fabricated), O (annealed), or H (strain-hardened).
Here's what the most common aluminum tempers mean for your project:
| Temper Code | Treatment Process | Effect on Strength | Effect on Formability | Typical Applications |
|---|---|---|---|---|
| T4 | Solution heat-treated and naturally aged at room temperature | Moderate increase (40-60% of T6) | Excellent—ideal for forming operations | Parts requiring post-extrusion bending, complex formed shapes |
| T5 | Cooled from extrusion temperature and artificially aged | Good increase (80-90% of T6) | Moderate—some forming still possible | Architectural profiles, standard structural applications |
| T6 | Solution heat-treated and artificially aged | Maximum strength for the alloy | Limited—bending may cause cracking | High-stress structural components, load-bearing frames |
| T651 | T6 plus stress relieved by stretching | Same as T6 | Limited—improved dimensional stability | Precision machined parts, aerospace components |
| T66 | Similar to T6 with tighter process controls | Higher than standard T6 | Limited | European structural standards, high-performance applications |
Notice how the same 6061 alloy can behave completely differently depending on its aluminium temper? A 6061-T4 extrusion bends readily for forming operations, while 6061-T6 resists deformation under heavy loads. This flexibility is precisely how aluminum extrusion is made suitable for such diverse applications.
What actually happens during heat treatment? The process manipulates the alloy's internal structure at the atomic level. During solution heat treatment, the extrusion is heated to temperatures around 980°F (527°C), causing alloying elements to dissolve into the aluminum matrix. Rapid cooling "freezes" these elements in place, creating a supersaturated solution.
Aging—whether natural (at room temperature) or artificial (in a controlled furnace)—allows these dissolved elements to precipitate out as microscopic particles that strengthen the material. The longer and hotter the aging process, the more completely this precipitation occurs.
Imagine you're specifying 6063 profiles for an architectural curtain wall. Should you choose T5 or T6 temper? This decision impacts more than just strength—it affects your budget and timeline.
The cost difference stems from processing complexity. T5 temper uses heat from the extrusion process itself—the profile exits the press hot and proceeds directly to artificial aging. T6 requires an additional solution heat treatment step before aging, adding furnace time, energy costs, and handling.
For applications where the aluminum temper chart shows T5 meets your mechanical requirements, you'll typically save 5-15% on material costs while reducing lead times by several days. However, when structural codes or stress calculations demand T6 properties, the additional investment ensures your profiles perform under load.
Consulting your extrusion supplier early in the design phase helps optimize this decision—they can advise whether T5 properties satisfy your requirements or if T6 is truly necessary for your application's safety margins.
You've identified the right alloy and temper for your application—but have you considered how easily that material actually flows through an extrusion die? Extrudability isn't just a manufacturing concern. It directly impacts what shapes you can create, how tight your tolerances can be, and ultimately, what you'll pay for your profiles. Understanding this often-overlooked factor can save you from costly design revisions and unexpected budget overruns.
Think of extrudability as a measure of how cooperatively an alloy behaves during the aluminum extrusion process. Some alloys flow smoothly through complex dies at high speeds, while others resist deformation, crack under pressure, or require specialized handling that drives up costs.
Why does 6063 glide through dies while 7075 aluminum extrusion presents significant challenges? The answer lies in metallurgical behavior at elevated temperatures. Several factors determine how well an alloy extrudes:
The magnesium-silicon combination in 6xxx alloys creates an ideal balance. These elements form compounds that facilitate smooth material flow without compromising the finished product's integrity. In contrast, the zinc and copper in 7xxx and 2xxx alloys increase strength but also raise flow stress and hot shortness susceptibility—making extrusion of aluminium in these grades considerably more challenging.
Following aluminum extrusion design guidelines becomes especially critical when working with less extrudable alloys. The same profile geometry that works perfectly in 6063 might prove impossible in 7075 without significant modifications.
The extrusion industry uses 6063 as the benchmark for extrudability—it's assigned a rating of 100%. All other alloys are measured against this standard. Here's how common alloys rank from easiest to most difficult:
What do these ratings mean for your aluminum extrusion design? More extrudable alloys enable thinner walls, sharper corners, tighter tolerances, and more intricate cross-sections. When you're working within aluminium extrusion design guidelines for complex profiles, staying with highly extrudable grades gives you maximum design freedom.
Extrudability directly correlates with production costs, creating distinct pricing tiers that every engineer should understand:
| Cost Tier | Typical Alloys | Cost Drivers | Design Flexibility |
|---|---|---|---|
| Economy | 6063, 6101, 1xxx series | Fast press speeds, standard dies, minimal scrap | Maximum—complex shapes, thin walls, tight tolerances |
| Mid-Range | 6061, 6005, 6082 | Moderate speeds, reinforced dies, controlled processing | Good—most standard profiles achievable |
| Premium | 7075, 2024, 7005 | Slow speeds, specialized dies, higher scrap rates, expert handling | Limited—simpler geometries, thicker sections |
This aluminum extrusion design guide principle applies universally: the harder an alloy is to extrude, the more you'll invest in tooling, processing time, and material waste. Premium-tier alloys might cost two to three times more per pound than economy options—and that's before factoring in increased die costs and longer lead times.
The practical takeaway? Never specify a difficult-to-extrude alloy unless your application truly demands its properties. If 6061 delivers adequate strength for your structural requirements, choosing 7075 "just to be safe" wastes money without adding value. Matching alloy capabilities precisely to application requirements—rather than over-engineering—is where smart aluminum extrusion design saves budget while maintaining performance.
Of course, selecting the right alloy for extrudability and strength is only part of the equation. Your choice also determines which surface finishing options will deliver the appearance and protection your application requires.
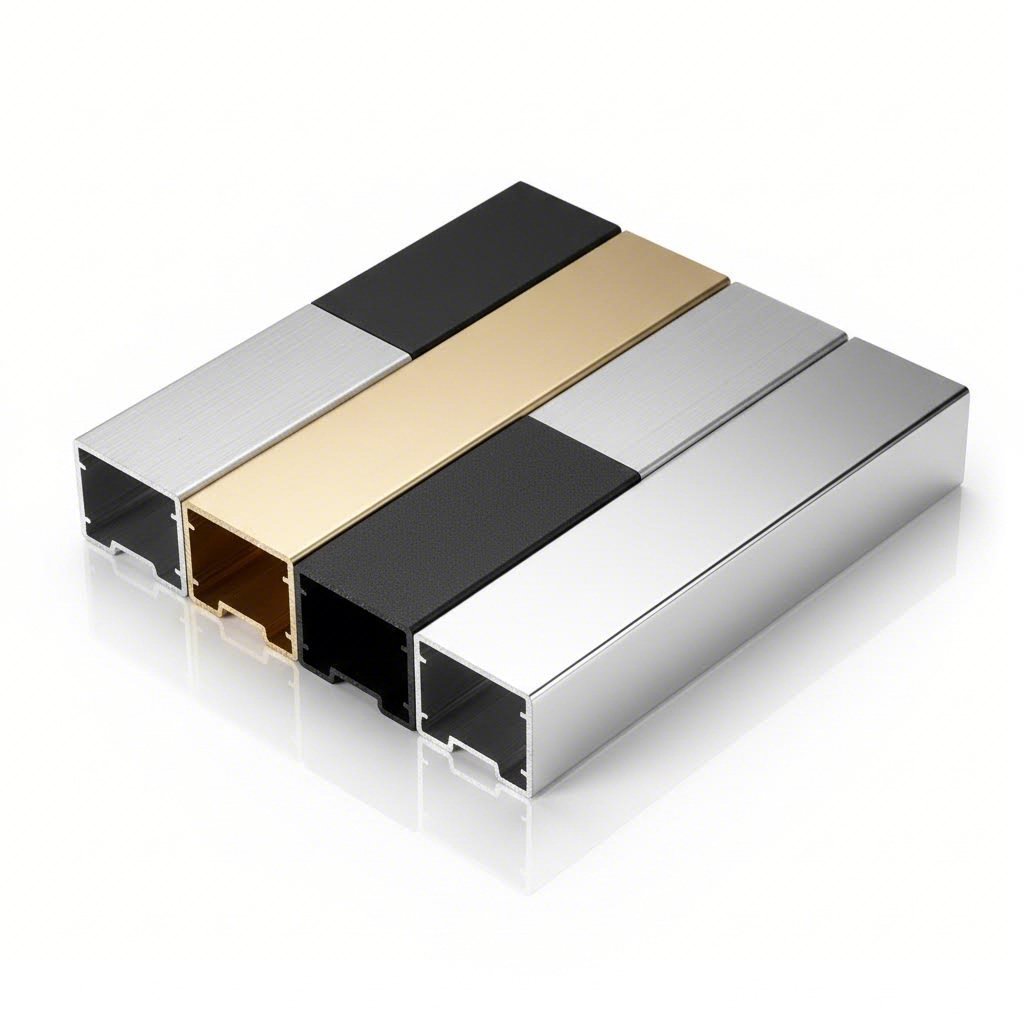
You've selected an alloy with the right strength and extrudability—but will it look the way you need it to? Surface finishing often determines whether your aluminum extrusion applications succeed in the real world. The alloy you choose fundamentally affects how well your profiles accept anodizing, powder coating, and other protective treatments. Ignore this relationship, and you might end up with inconsistent finishes, premature corrosion, or costly rework.
Here's what many engineers discover too late: not all alloys respond equally to surface treatments. The same anodizing process that produces a flawless architectural finish on 6063 can yield disappointing results on 6061. Understanding why this happens—and how to match alloys to your finishing requirements—prevents these frustrating surprises.
Each finishing method interacts differently with aluminum's surface chemistry. The alloying elements that boost strength or improve extrudability can work for or against your finishing goals. Consider this comparison of how standard aluminum extrusions perform across common finishing methods:
| Finishing Method | 6063 | 6061 | 6005 | 6082 | Key Considerations |
|---|---|---|---|---|---|
| Anodizing | Excellent | Good | Good | Moderate | Copper content affects uniformity; lower is better |
| Powder Coating | Excellent | Excellent | Excellent | Excellent | Proper pretreatment essential for all alloys |
| PVDF Coating | Excellent | Good | Good | Good | Surface preparation determines adhesion quality |
| Painting | Excellent | Excellent | Excellent | Excellent | Minimal alloy sensitivity with proper primers |
| Mechanical Finishing | Excellent | Good | Good | Good | Harder alloys may show more visible scratches |
What explains these differences? During anodizing, a protective oxide layer forms on the aluminium extrusion surface through an electrochemical process. This layer improves both corrosion resistance and appearance. However, according to research presented at the 2024 Aluminum Extrusion Technology Seminar, trace elements in the alloy—particularly zinc, copper, and manganese—significantly influence how uniformly this oxide layer develops.
Walk past any modern building with aluminum window frames, curtain walls, or decorative trim. Chances are you're looking at 6063 extruded aluminium. This alloy's dominance in architectural applications stems directly from its superior finishing characteristics.
The secret lies in 6063's chemical composition. With copper content limited to just 0.10% maximum, this alloy produces exceptionally uniform anodized finishes. Higher copper levels—like those found in 6061—can cause uneven coloring and surface inconsistencies that become obvious on large architectural panels.
Research confirms that zinc concentrations above 0.025% can cause preferential grain etching (PGE) during the alkaline etching step before anodizing. This creates a condition where some grains etch deeper than others, resulting in a mottled or streaky appearance. The study found that adding small amounts of copper actually helps prevent this PGE effect—but too much copper creates its own problems with color consistency.
Interestingly, temper also plays a role. Alloys in T4 temper show slightly higher tendency for preferential grain etching and produce more glossy surfaces compared to T6 or T7 tempers. If your aluminum flexibility requirements allow, specifying T6 temper can improve anodizing consistency.
Good news for powder coating applications: alloy selection matters less here than with anodizing. The same research demonstrated that filiform corrosion resistance of 6060 aluminum alloy profiles was not significantly affected by small variations in chemical composition, including copper content. When recommended pretreatment methods are applied—specifically achieving an etch rate of approximately 2 grams per square meter—all tested alloys met Qualicoat quality requirements.
The critical factor? Proper pretreatment. Researchers observed corrosion only in regions that were accidentally not chemically treated. This underscores a crucial point: surface preparation matters more than alloy chemistry for powder-coated applications.
For projects requiring both round aluminum extrusion profiles and flat architectural panels with powder coating, you have considerable alloy flexibility. The decision can prioritize mechanical properties or extrudability rather than finishing compatibility.
Corrosion resistance varies meaningfully across alloy grades, especially in harsh environments:
When specifying aluminum extrusion alloys for visible, long-term exterior applications, the combination of 6063 base material with appropriate surface treatment delivers the best balance of appearance, durability, and cost-effectiveness. Understanding which alloy works best with your required finish prevents specification errors that compromise either aesthetics or performance.
Now that you understand alloy properties, tempers, extrudability, and finishing compatibility, how do you apply all this knowledge to your specific project? The answer depends heavily on your industry. A window frame manufacturer faces completely different requirements than an aerospace engineer designing aircraft components. Let's translate everything you've learned into practical, industry-specific guidance for aluminum extrusions.
Each industry prioritizes different characteristics. Architects demand flawless surface finishes. Automotive engineers obsess over weight reduction. Aerospace applications require extreme strength-to-weight ratios. Understanding these priorities helps you navigate directly to the right alloy without wading through irrelevant options.
When you're designing curtain walls, window systems, storefronts, or decorative facades, aesthetics matter as much as performance. This is where types of extruded aluminum diverge most dramatically from industrial applications.
6063 aluminum dominates architectural work for compelling reasons. Its exceptional extrudability allows manufacturers to create intricate decorative profiles with thin walls and sharp details. The alloy's low copper content produces uniform anodized finishes that maintain consistent appearance across large building facades. For aluminum frame extrusion applications like window and door systems, 6063-T5 or T6 delivers the ideal combination of formability, corrosion resistance, and visual appeal.
What about secondary operations? Architectural profiles frequently require:
For small aluminum extrusions used in trim, decorative accents, or hardware, 6063 remains the standard. Its fine grain structure and excellent surface response ensure even the smallest aluminium extrusion parts meet demanding aesthetic requirements.
Beyond architecture, high-performance aluminum extrusions industrial applications demand alloys optimized for strength, durability, or specialized operating conditions. Here's where understanding extruded aluminum shapes and their material requirements becomes critical.
Use this decision framework to match your industry requirements to the optimal alloy selection:
| Industry/Application | Recommended Alloys | Key Requirements | Critical Considerations |
|---|---|---|---|
| Aerospace - Structural | 7075, 7050, 2024 | Maximum strength-to-weight ratio, fatigue resistance, damage tolerance | Limited extrudability restricts profile complexity; corrosion protection essential; higher material and tooling costs |
| Aerospace - Non-structural | 6061, 6063 | Good strength, formability, corrosion resistance | Suitable for interior components, ducting, non-critical structural elements |
| Automotive - Structural | 6061, 6082, 6005 | Crash energy absorption, weldability, lightweighting | Heat treatment affects crash performance; consider post-weld strength reduction in design |
| Automotive - Trim/Decorative | 6063 | Surface finish quality, corrosion resistance | Excellent for visible components; anodizing or powder coating recommended |
| Marine | 5083, 5086, 6063 | Saltwater corrosion resistance, weldability | 5xxx series excels in hull applications; avoid copper-containing alloys; anodizing enhances protection |
| Rail/Transit | 6005, 6082, 6061 | Structural integrity, fatigue resistance, weldability | European standards often specify 6082; consider crash energy requirements for car body structures |
| Industrial Machinery | 6061, 6082 | Machinability, strength, dimensional stability | T651 temper preferred for precision-machined components; excellent thread-cutting characteristics |
| Heat Exchangers | 6063, 3003, 1100 | Thermal conductivity, corrosion resistance, formability | Thin-wall capability essential; brazing compatibility may influence selection |
Aerospace applications represent the most demanding use cases for aluminum extrusions. The 7xxx series—particularly 7075—delivers tensile strength approaching 83,000 psi, rivaling many steel alloys at a fraction of the weight. According to Silver City Aluminum, 7075 is renowned for its extraordinary strength and is often utilized in high-performance applications such as aerospace components and athletic gear.
However, these high-performance alloys introduce manufacturing challenges. Their poor extrudability limits profile complexity, requiring simpler geometries and thicker wall sections. Secondary operations require special attention:
The automotive industry's push for fuel efficiency and electric vehicle range has made aluminum extrusions increasingly valuable. The 6xxx series offers the ideal balance for most automotive applications—adequate strength with excellent formability and weldability.
6061 and 6082 dominate structural applications like crash management systems, subframes, and battery enclosures. These alloys absorb impact energy effectively while welding readily for complex assemblies. For decorative trim, bumper accents, and roof rails, 6063 delivers the surface quality customers expect.
When designing automotive aluminium extrusion parts, remember that welded joints lose approximately 30% of their heat-treated strength. Either oversize joints to compensate, or specify post-weld heat treatment to restore properties—a common practice for safety-critical components.
With clear understanding of which alloys serve which industries, you're equipped to make informed selections. But even the right alloy choice can go wrong without careful attention to common specification pitfalls that trip up even experienced engineers.
You've invested time understanding alloy properties, temper designations, and industry requirements—but knowledge alone doesn't prevent costly errors. Even experienced engineers fall into predictable traps when specifying aluminum extrusion material. The consequences? Inflated budgets, delayed timelines, failed parts, and frustrating rework. Let's examine the most common mistakes so you can avoid them entirely.
What are aluminum extrusions actually costing you when specifications go wrong? Often far more than the material itself. Incorrect alloy choices cascade into tooling modifications, production delays, surface finishing problems, and field failures that dwarf the original part cost. Understanding these pitfalls transforms you from someone who simply selects alloys into an engineer who optimizes every project from the start.
After reviewing countless specification errors across industries, clear patterns emerge. Here are the most expensive and common mistakes engineers make when selecting types of aluminum extrusions:
Preventing these mistakes requires a systematic approach rather than relying on habit or assumption. The key insight from Ulbrich's alloy selection guide applies directly here: "Many aspects need to be considered in alloy selection and they are not always weighted evenly." Different stakeholders—purchasing, engineering, production—evaluate factors differently, and all perspectives matter.
Before finalizing any aluminum extrusion types specification, work through this decision checklist:
The most successful projects balance all these factors systematically rather than optimizing for any single characteristic. As one industry resource notes, alloy selection requires weighing physical properties, mechanical properties, cost, service life, fabrication requirements, and surface properties together—not in isolation.
With a clear understanding of what to avoid and a systematic approach to specification, you're equipped to select alloys confidently. But even perfect specifications require the right manufacturing partner to translate your designs into reality.
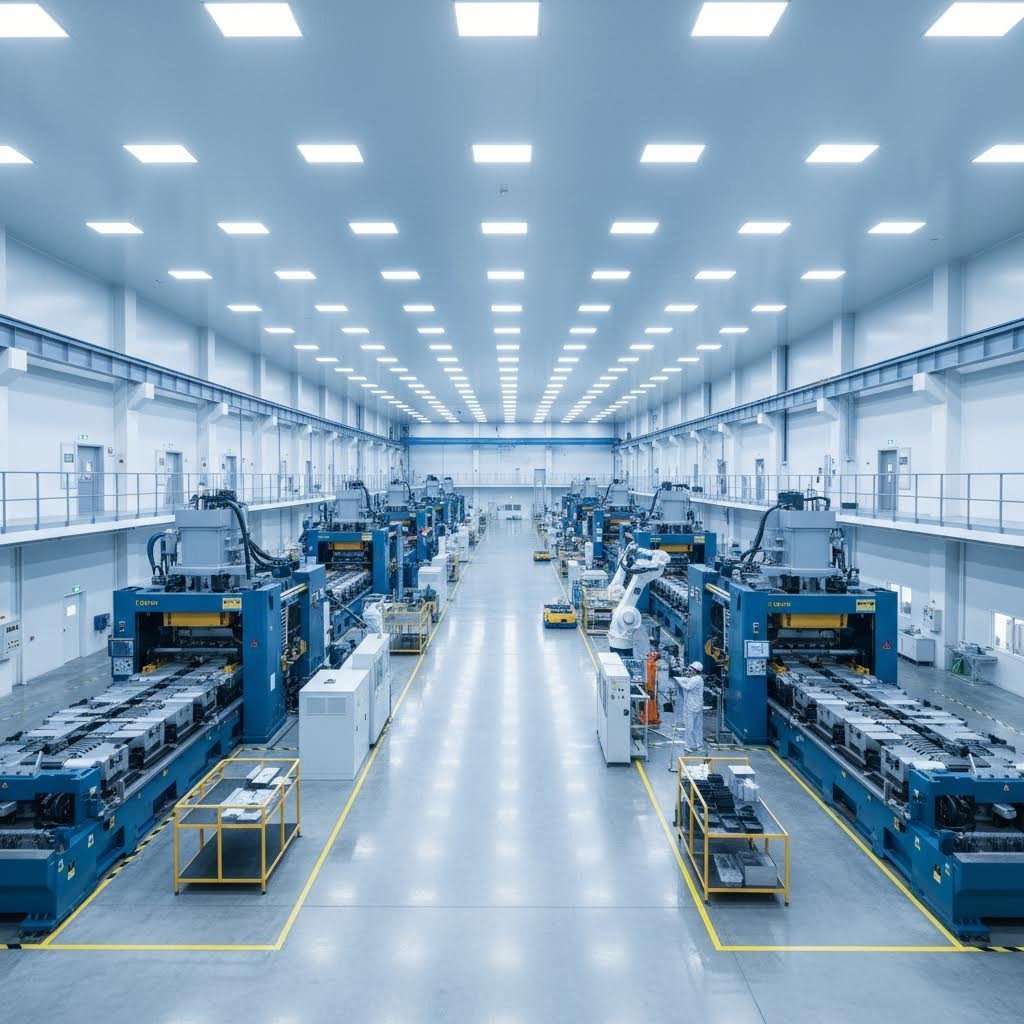
You've selected the perfect alloy, specified the right temper, and designed a profile optimized for extrudability. But here's the reality: even flawless specifications fail without a capable manufacturing partner. The aluminum extrusion die that shapes your profile, the press that forces material through it, and the finishing lines that protect it—all of these determine whether your project succeeds or stumbles. Choosing the right supplier isn't just a procurement decision; it's a technical one that directly impacts quality, cost, and delivery.
How do you distinguish a truly capable aluminum extrusion manufacturing partner from one that simply claims capability? The answer lies in evaluating specific technical competencies that experienced engineers know to examine closely.
When sourcing custom aluminum profile extrusion, supplier capability extends far beyond competitive pricing. According to industry best practices from Aluphant's supplier evaluation guide, procurement teams should assess multiple technical dimensions before committing to a manufacturing relationship.
Here are the essential criteria for evaluating potential suppliers:
The best aluminum extrusion tooling means nothing without effective collaboration throughout your project lifecycle. Strong suppliers differentiate themselves through technical communication and proactive problem-solving.
What should you expect from a capable partner?
For example, Shengxin Aluminium demonstrates what comprehensive capability looks like in practice: 35 extrusion presses spanning 600T to 5500T capacity, integrated CNC machining centers for precision cutting, drilling, and bending, plus complete surface treatment lines offering anodizing, powder coating, PVDF, and micro-arc oxidation. This end-to-end approach—from die development through mass production and finishing—represents the benchmark for evaluating potential suppliers. You can explore their deep processing capabilities as a reference point for what integrated aluminum profile extrusion services should include.
Capability means little if delivery windows slip repeatedly. According to industry benchmarks, typical lead times for standard projects break down as follows:
Ask prospective suppliers how they manage production scheduling during peak seasons. Factories using ERP-based production systems generally deliver more consistently than those relying on informal planning methods.
Ultimately, your extrusion supplier becomes an extension of your engineering team. The right partner doesn't just manufacture what you specify—they help you specify what works best. By evaluating press capabilities, die expertise, finishing options, quality systems, and communication practices systematically, you'll identify partners who consistently deliver aluminum extrusion manufacturing results that meet your requirements on time and within budget.
6063 aluminum is widely considered the best alloy for extrusion due to its excellent extrudability rating (100% benchmark), superior anodizing response, and ability to form complex thin-wall profiles. It dominates architectural applications like window frames and curtain walls. However, the 'best' alloy depends on your requirements—6061 offers higher strength for structural applications, while 6082 provides enhanced fatigue resistance for demanding industrial uses.
Yes, 6061 aluminum is one of the most popular extruded aluminum alloys on the market. While it has slightly lower extrudability than 6063 (rated approximately 70-90% versus 100%), it's routinely extruded for structural applications requiring higher tensile strength (45,000 psi in T6 temper). 6061 is commonly used in automotive components, aerospace parts, machinery frames, and load-bearing structural profiles where strength takes priority over surface finish quality.
The key differences lie in composition and performance. 6061 contains more copper (0.15-0.4%) and magnesium (0.8-1.2%), delivering approximately 29% higher tensile strength than 6063. However, 6063's lower copper content (0.10% max) produces superior anodized finishes and better corrosion resistance. Choose 6063 for architectural aesthetics and complex profiles; select 6061 when structural strength, machining, or fatigue resistance matters most.
Temper designations (T4, T5, T6, T651) indicate heat treatment conditions that transform mechanical properties. T4 offers excellent formability with moderate strength—ideal for post-extrusion bending. T5 provides good strength (80-90% of T6) at lower cost since it uses extrusion heat directly. T6 delivers maximum strength but limited formability. T651 adds stress relief for precision-machined components. Choosing T5 over T6 when adequate can save 5-15% on material costs.
Evaluate press capacity range (small to large tonnage for profile flexibility), in-house die design and manufacturing capabilities, integrated CNC machining centers for precision finishing, comprehensive surface treatments (anodizing, powder coating, PVDF), quality certifications (ISO 9001, EN755-9), and technical support from design through production. Partners like Shengxin Aluminium with 35 presses (600T-5500T) and end-to-end processing demonstrate the comprehensive capabilities that ensure consistent quality and shorter lead times.


 un service en ligne
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 français
 English
 Deutsch
 русский
 español
 português
 العربية
 ไทย
 Việt
 Українська