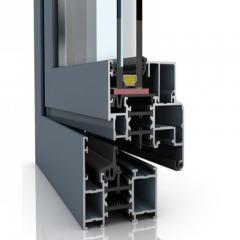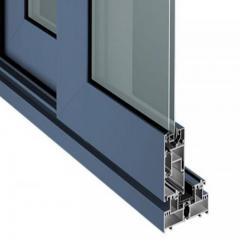
When you're sourcing extruded aluminum for your next project, understanding who you're working with matters just as much as the profiles themselves. Aluminum extrusion vendors serve as the critical link between raw material production and your finished components. But here's the challenge: not all vendors offer the same capabilities, and choosing the wrong partner can derail your project timeline and budget.
So what exactly separates aluminum extrusion companies from distributors or dealers? True manufacturers operate extrusion presses and control the entire production process, from billet heating to surface treatment. According to industry experts, genuine manufacturers invest in extrusion equipment, surface treatment workshops, and even sewage treatment facilities for proper wastewater disposal. Distributors, on the other hand, purchase profiles from manufacturers and provide value-added services like cutting, machining, and assembly.
Imagine you need a custom aluminum profile for an industrial building system. Should you contact a manufacturer or a dealer? Manufacturers excel at custom extrusions and large-volume orders, often requiring minimum quantities since they produce to order rather than stocking inventory. Aluminum extrusion suppliers who operate as dealers typically maintain stock for smaller, scattered orders and offer quicker turnaround for standard shapes. Understanding this distinction helps you approach the right partner for your specific needs.
The aluminum extrusion supply chain involves multiple stages: die development, extrusion pressing, heat treatment, surface finishing, and fabrication. Each stage presents opportunities for quality control or potential delays. Lead times for new projects can stretch to 16 weeks for simple designs, and complex designs with fabrication and anodizing may require 20 weeks or longer.
The right vendor partnership isn't about finding the lowest price per pound. It's about finding a partner whose capabilities, communication style, and quality standards align with your project requirements.
This guide takes a buyer-centric approach, helping you evaluate vendors based on what genuinely matters for project success. You'll learn to ask informed questions, compare capabilities objectively, and build partnerships that deliver consistent quality over time.
Ever wonder why one vendor can produce your complex aluminum profile while another turns you away? The answer lies in understanding how aluminum extrusions are actually made. When you grasp the fundamentals of the extrusion process, you'll ask smarter questions and quickly identify which suppliers can truly meet your specifications.
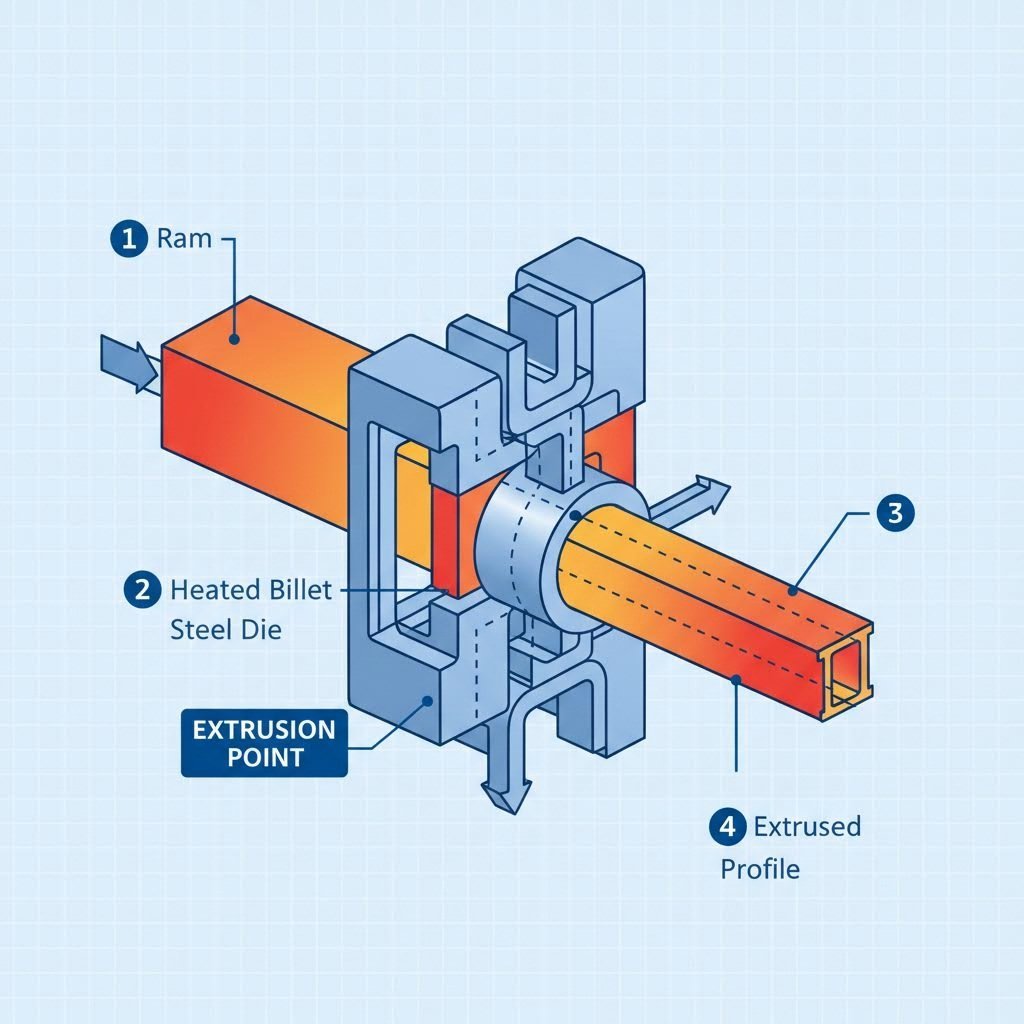
Think of aluminum extrusion like squeezing toothpaste through a shaped nozzle, except the "toothpaste" is solid aluminum heated to around 800-925°F, and the "nozzle" is a precision-engineered steel die. The process transforms cylindrical aluminum billets into complex aluminum extrusion profiles with consistent cross-sections.
Here's how the journey unfolds:
According to Bonnell Aluminum's technical resources, temperature control throughout this process is the most critical factor, directly affecting characteristics like hardness and surface finish.
Not all extrusion presses are created equal. Press size determines the maximum dimensions of profiles a vendor can produce, measured by the largest circle that can completely enclose the profile's cross-section. This is called the circumscribing circle.
When evaluating vendors, consider how press tonnage affects your options:
| Press Capacity | Typical Applications | Profile Characteristics |
|---|---|---|
| Small (under 1,500 tons) | Small aluminum extrusions, aluminum angle, precision components | Tighter tolerances on smaller shapes |
| Medium (1,500-4,000 tons) | Aluminum square tubing, standard architectural profiles | Balance of size and precision |
| Large (4,000+ tons) | Large structural sections, industrial applications | Maximum cross-sectional dimensions |
Vendors with multiple press lines offer greater flexibility. If one press is dedicated to a large order, alternative presses can handle your project without delays. This redundancy also provides backup capacity during maintenance periods.
The die is where your aluminum profile design becomes reality. Think of it as the DNA of your extrusion, determining everything from wall thickness to the complexity of hollow sections. Vendors with strong die development expertise can advise you on design modifications that improve extrudability while maintaining your functional requirements.
Several technical factors influence whether a vendor can successfully produce your profile:
When it comes to alloy selection, your application requirements should drive the choice. Alloy 6063 is the architectural workhorse, offering excellent extrudability and surface finish for applications like window frames and decorative trim. Alloy 6061 delivers higher strength with a tensile strength of 310 MPa when heat-treated to T6 temper, making it ideal for structural applications, flex pipe connections, and components requiring superior mechanical properties.
Understanding these process fundamentals transforms how you evaluate potential vendors. You'll recognize when a supplier genuinely understands your requirements versus when they're simply taking orders. This technical foundation prepares you to assess the specific capabilities that truly differentiate good vendors from great ones.
Now that you understand how the extrusion process works, it's time to translate that knowledge into practical evaluation criteria. When comparing aluminum extrusion vendors, the technical capabilities they bring to the table directly determine whether your project succeeds or stumbles. Let's break down exactly what to look for and how to match your specifications with the right supplier.
Think of press capacity as the first filter in your vendor evaluation. A supplier might offer excellent service and competitive pricing, but if their equipment can't produce your aluminum extrusion profile dimensions, none of that matters.
Press tonnage determines the force available to push aluminum through the die. Larger, more complex extruded aluminum profiles require higher tonnage. But here's what many buyers overlook: it's not just about having enough power. The relationship between press capacity and your profile's circumscribing circle size affects everything from wall thickness consistency to surface quality.
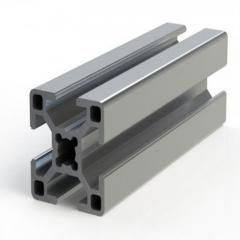
When you're working with popular modular framing profiles like 4040 aluminum extrusion or 3030 aluminum extrusion systems, most medium-capacity vendors can handle production. However, if your project involves large structural sections or extruded aluminum rails with intricate cross-sections, you'll need to verify the vendor operates presses in the 4,000+ ton range.
Here's a comprehensive comparison table to help you evaluate vendor capabilities against your project requirements:
| Capability Factor | Entry-Level Vendor | Mid-Tier Vendor | Premium Vendor |
|---|---|---|---|
| Press Tonnage Range | 500-1,500 tons | 1,500-4,000 tons | 4,000-10,000+ tons |
| Maximum Profile Width | Up to 6 inches | Up to 12 inches | Up to 20+ inches |
| Maximum Circumscribing Circle | Up to 8 inches | Up to 14 inches | Up to 20+ inches |
| Wall Thickness Tolerance | ±0.010" standard | ±0.007" achievable | ±0.005" precision |
| Secondary Processing | Cutting only | Cutting, drilling, basic machining | Full CNC, bending, welding, assembly |
| Die Turnaround Time | 4-6 weeks | 2-4 weeks | 1-3 weeks (with expedite options) |
Sounds complex? It doesn't have to be. Tolerance specifications essentially tell you how precisely a vendor can produce your aluminum extrusion shapes. Understanding industry standards helps you set realistic expectations and identify vendors who can genuinely meet your requirements.
According to dimensional tolerance data from Methode Power Solutions, standard commercial tolerances follow specific guidelines established by the Aluminum Association. These tolerances depend on two factors: the dimension size and the die's circle size. For example:
Flatness tolerance is equally important, particularly for custom aluminum extrusions used in precision assemblies. The base flatness specification depends on both the surface width and the metal thickness forming that surface. Thicker walls generally achieve better flatness, with tolerances as tight as 0.004" per inch of width for sections over 2" thick.
When you're evaluating vendors, ask these specific questions:
Here's where good vendors separate themselves from great ones. The extrusion itself is just the beginning. Most projects require secondary processing: cutting to length, drilling holes, machining features, bending curves, or adding surface treatments. Vendors with integrated deep processing capabilities can streamline your supply chain dramatically.
As noted by Sino Extrud's technical analysis, extruded aluminum works exceptionally well with CNC processing. The uniform cross-section and stable metal structure allow for clean cuts and predictable outcomes. Profiles exit the extrusion process with much of the geometry already formed, so CNC operations focus on precise holes, slots, and cutouts rather than bulk material removal.
When evaluating CNC capabilities, consider these factors:
The compatibility between extrusion and CNC processing creates a powerful hybrid approach. Vendors who understand this can help you optimize your profile design for manufacturability. For instance, building slots, channels, or mounting features directly into the extrusion reduces subsequent machining time and cost.
However, recognize the limitations. According to industry experience, thin-walled extruded aluminum profiles can deform under aggressive CNC milling. If your design requires deep pockets or features machined into walls under 0.125" thick, discuss this specifically with potential vendors. The best partners will advise you honestly about what's achievable versus what risks part rejection.
Die development expertise deserves special attention in your evaluation. A vendor with strong die design capabilities can suggest modifications that improve extrudability without compromising your functional requirements. Ask about their die library, turnaround time for new dies, and whether they offer die cost amortization programs for larger orders.
When requesting quotes for custom aluminum extrusions, include your complete processing requirements upfront. This allows vendors to provide accurate pricing and realistic timelines. A vendor who can handle extrusion, machining, and finishing under one roof eliminates coordination headaches and reduces your total lead time compared to managing multiple suppliers.
With a clear understanding of technical capabilities, you're ready to explore the surface treatment options that complete your extruded aluminum profiles and determine their final appearance and performance characteristics.
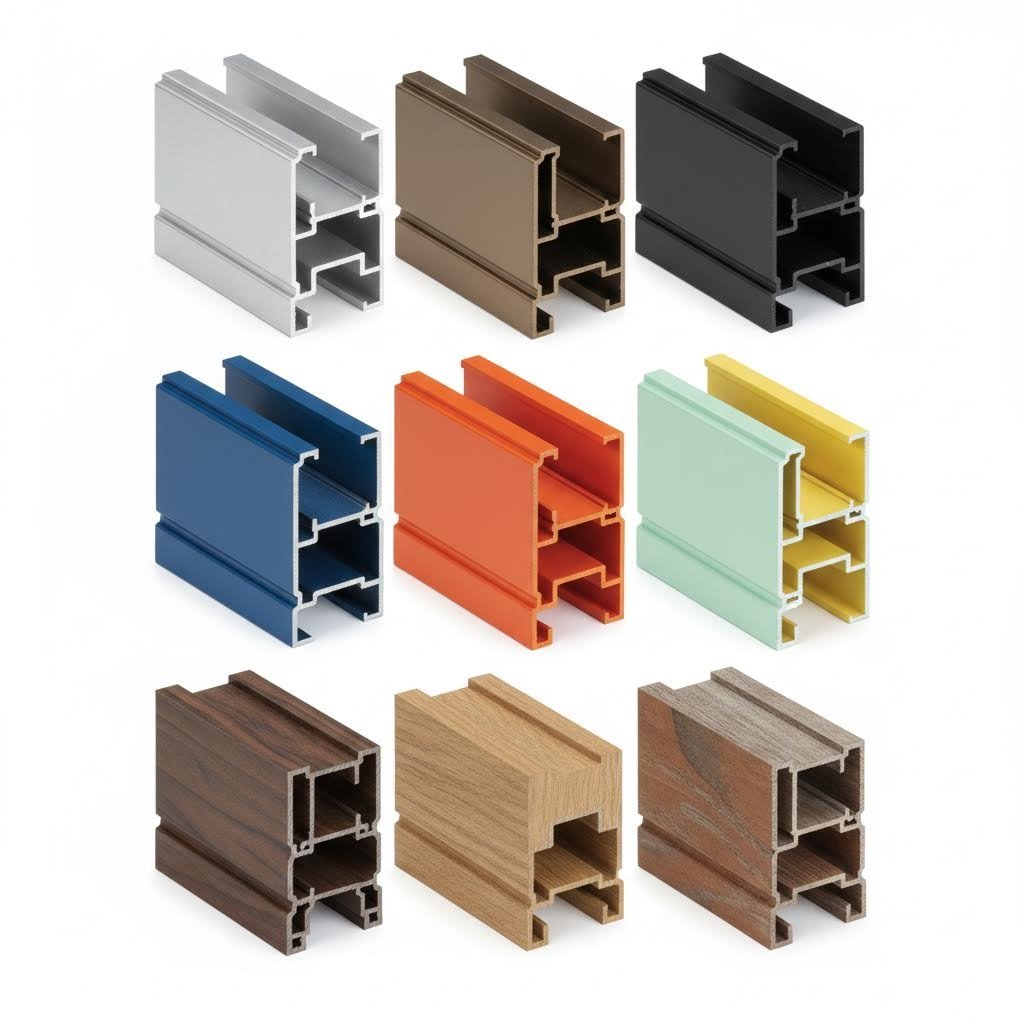
You've evaluated press capacity and machining capabilities, but here's something many buyers overlook: the surface finish can make or break your aluminum extrusion project. The right surface treatment transforms raw aluminum profiles into components that resist corrosion, match your brand aesthetics, and perform reliably for decades. Understanding your options helps you identify which vendors truly deliver complete solutions.
Surface treatments for anodized aluminum extrusions and other aluminium profile types fall into several categories. Here are the most common finishing options offered by quality vendors:
When most people picture anodized aluminum, they imagine that familiar silver-gray finish. But modern anodizing technology offers far more versatility than you might expect. The process works by enhancing aluminum's natural oxide layer through an electrochemical bath, creating a coating that's integral to the metal itself.
According to BWC Profiles' surface treatment guide, the anodizing process produces a protective oxide film that doesn't flake or peel away because it grows from the base aluminum rather than sitting on top of it. This makes anodizing particularly effective for aluminum extrusion trim applications where durability matters.
Consider these anodizing variations when evaluating vendors:
Coating thickness directly determines durability. As SAF's technical analysis explains, the lifetime of an anodic finish is proportional to its thickness. Class I coatings (0.7 mils) last approximately twice as long as Class II (0.4 mils) in exterior applications. When specifying aluminium extrusion trim for architectural use, always confirm the coating class to avoid premature degradation.
If you need color options beyond what anodizing offers, powder coating opens up virtually unlimited possibilities. This dry finishing process electrostatically applies finely ground pigment and resin powder to your aluminum profiles, then cures the coating under heat to create a smooth, continuous film.
Why does powder coating dominate so many applications? The advantages are compelling:
However, powder coating has limitations worth understanding. According to Cast-Mold's finishing guide, proper pretreatment is essential when powder coating cast or extruded aluminum. The surface must be degassed and prepared correctly, or porosity can cause blisters during the heat curing process. This is why vendors with in-house finishing typically achieve better results than those outsourcing to third parties.
Some projects require performance characteristics that standard anodizing or powder coating can't deliver. This is where specialty finishes differentiate capable vendors from basic suppliers.
PVDF coatings (polyvinylidene fluoride) represent the premium choice for exterior architectural applications. These fluoropolymer coatings offer exceptional UV resistance and color stability, explaining their dominance in curtainwall and metal roofing markets. PVDF formulations typically blend 70% PVDF resin with 30% acrylics, meeting the stringent AAMA 2605 specification that requires actual ten-year South Florida exposure testing.
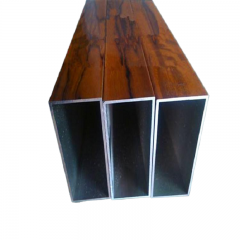
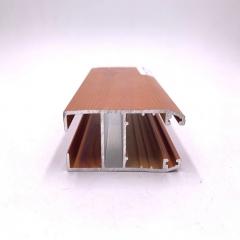
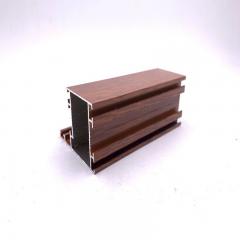
Wood grain finishes provide an alternative worth considering for projects blending modern performance with traditional aesthetics. Profile wrapping techniques apply thin wood veneer or printed foils to aluminum surfaces, creating profiles that look like natural wood while delivering aluminum's durability and dimensional stability.
When evaluating vendors on finishing capabilities, ask these critical questions:
Vendors with in-house finishing provide distinct advantages in quality control and lead times. When extrusion and finishing happen under one roof, there's no coordination delay between suppliers, no shipping damage to raw profiles, and immediate accountability if issues arise. Your RFQ documents should specify the exact finish required, including color codes, gloss levels, coating thickness, and any applicable performance standards like AAMA 2605 for spray coatings.
With finishing capabilities understood, you're ready to navigate the RFQ process itself and learn how to structure inquiries that generate meaningful vendor comparisons.
You've identified what to look for in aluminum extrusion vendors, but now comes the moment of truth: actually requesting quotes and evaluating responses. The RFQ process reveals more about a potential partner than any marketing brochure ever could. How vendors respond to your inquiry, what questions they ask, and how quickly they provide accurate information all signal whether they'll perform reliably during production.
Imagine sending a vague RFQ to five vendors and receiving five wildly different quotes. Without standardized information, you're comparing apples to oranges. A well-prepared request for quote eliminates this confusion and demonstrates that you're a serious buyer worth prioritizing.
According to industry procurement guidance, structuring your RFQ properly drives comparable quotes and reveals each vendor's true capabilities. Here's your complete preparation checklist:
When preparing your custom aluminum extrusion RFQ, include a sample-approval timeline with clear milestones. This sets expectations upfront and helps vendors propose realistic schedules rather than overpromising to win the business.
Here's something many buyers overlook: the quality of your RFQ directly influences the quality of responses you receive. Vendors need specific information to provide accurate pricing and realistic timelines for aluminum extrusion services.
For custom extrusion aluminum projects, suppliers must understand your profile's complexity before quoting. According to qualification best practices, key information includes the circumscribing circle size, wall thickness variations, and any semi-hollow features that affect die design difficulty. Without this data, vendors either pad quotes with contingencies or underestimate costs that surface later.
Consider providing these additional details to generate meaningful comparisons:
For profile custom extrusions requiring tight tolerances, request that vendors include their tolerance matrices and capability data in their responses. This prevents surprises during production when you discover a vendor quoted standard tolerances but can't actually achieve your precision requirements.
The quote phase is essentially an extended interview. How vendors respond reveals their professionalism, technical depth, and communication style. Pay attention to these signals when evaluating responses.
Green lights that indicate a strong partner:
Red flags that warrant caution:
According to procurement research, proactively addressing communication bottlenecks during the RFP process can lead to 97 percent fewer delays. Vendors who respond promptly and thoroughly during the quote phase typically maintain that responsiveness throughout production.
When evaluating samples and prototypes, establish clear acceptance criteria upfront. A professional aluminum extrusion supplier provides dimensional inspection reports covering cross-sectional accuracy, wall thickness data, flatness, and perpendicularity. Request samples from both ends and the middle of extrusion runs to verify uniformity. For profile precision extrusions with tight tolerances, ask vendors to demonstrate their measurement capabilities using CMM, laser scanners, or profile projectors.
The quote phase also reveals how vendors handle the qualification process. According to extrusion qualification guidelines, a structured approach includes die trials, dimensional verification, machining compatibility checks, and surface treatment evaluation before mass production approval. Vendors who propose this methodical approach demonstrate commitment to quality rather than rushing to production.
With your RFQ process refined and vendor responses evaluated, you're ready to assess whether potential partners can scale with your production demands and maintain supply chain reliability over time.
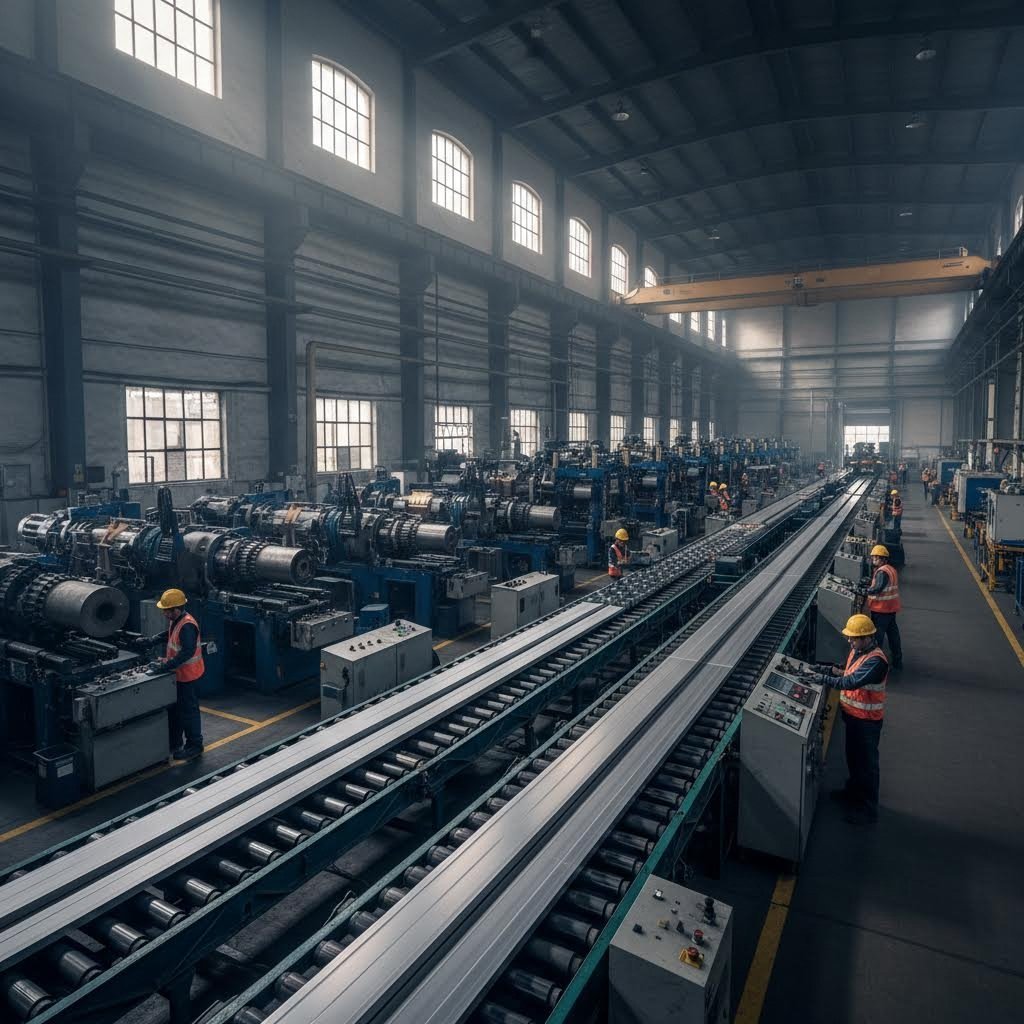
You've identified vendors with the right technical capabilities and finishing options, but here's a question that often catches buyers off guard: can this partner actually deliver when you need to scale up? A vendor might produce exceptional aluminum extrusion supply for your initial order, yet completely buckle under increased demand. Understanding production capacity and scalability separates partners who support your growth from those who become bottlenecks.
Think about your project timeline. You need 500 profiles for prototyping next month, then potentially 10,000 units per quarter once production ramps. Can your vendor handle both scenarios without sacrificing quality or delivery dates?
Production capacity depends heavily on equipment infrastructure. According to industry capability assessments, extrusion companies with multiple press capacities can handle a wider range of projects and maintain flexibility when production volumes change. A vendor operating a single press line faces obvious constraints: maintenance downtime halts everything, and competing orders create scheduling conflicts.
When evaluating extrusion companies for capacity, consider these factors:
For products like 8020 aluminum framing systems or aluminum tubing that require consistent availability, ask vendors about their typical lead times during peak versus slow seasons. The difference reveals how capacity constraints affect real-world delivery.
Imagine your product takes off. Orders double, then triple. Will your vendor celebrate with you or become your biggest headache? Scalability isn't just about current capacity; it's about a vendor's ability and willingness to grow alongside your business.
According to production scaling research, planning for scalability should begin early to avoid costly surprises down the line. The same principle applies to vendor selection. Partners with established capacity expansion strategies, whether through additional equipment investment or strategic partnerships, offer more security than those operating at maximum output.
Here are key questions to ask about scalability:
Vendors who discuss these questions openly demonstrate operational maturity. Those who deflect or provide vague assurances may struggle when your growth tests their limits.
Production capacity matters little if raw materials don't arrive on time or quality systems fail under pressure. Supply chain reliability involves multiple interconnected factors that separate dependable partners from risky ones.
As noted by manufacturing reliability experts, reliable suppliers work with a variety of alloys and maintain controlled billet inventory. Poor billet preparation leads to surface defects, dimensional drift, or extrusion line marks that compromise your final product. Vendors who source billets from certified mills and maintain proper homogenization and preheating controls deliver more consistent results.
Evaluate these supply chain stability indicators when comparing vendors:
Quality management systems provide another reliability indicator. According to supplier evaluation criteria, professional aluminum extrusion manufacturers should provide ISO 9001 certification at minimum, with industry-specific certifications like IATF 16949 for automotive or AS9100 for aerospace applications where applicable. These certifications demonstrate commitment to process control and traceability, vital attributes for long-term manufacturing partnerships.
Typical lead time benchmarks offer useful reference points for planning:
Vendors with integrated operations, handling extrusion, machining, and finishing under one roof, typically deliver shorter and more predictable lead times than those coordinating multiple subcontractors. This integration also simplifies accountability when issues arise.
Understanding production capacity and supply chain reliability prepares you to make informed decisions about vendor sourcing models, whether that means domestic suppliers, international manufacturers, or factory-direct partnerships that combine competitive pricing with comprehensive capabilities.
You've evaluated technical capabilities, finishing options, and production capacity. Now comes a strategic decision that shapes your entire supply chain: where should you source your aluminum extrusions? The choice between domestic suppliers, international custom aluminum extrusion manufacturers, and factory-direct partnerships involves trade-offs that extend far beyond per-piece pricing. Understanding these models helps you build vendor relationships that deliver value for years, not just one purchase order.
When buyers first explore sourcing options, the domestic versus international debate typically dominates the conversation. Both paths offer distinct advantages depending on your priorities, and neither represents a universally superior choice.
According to industry sourcing guidance, domestic aluminum profile extrusion suppliers provide shorter lead times, easier communication, and simplified logistics. You're working within the same time zone, speaking the same language, and avoiding customs complications. For rush orders or projects requiring frequent design iterations, these factors often outweigh cost considerations.
However, domestic sourcing typically comes with higher per-unit costs. Extruded aluminum manufacturers operating in North America or Europe face elevated labor, energy, and regulatory compliance expenses that translate directly to your quotes.
International sourcing flips this equation. Custom aluminum extrusion companies based in manufacturing hubs like China often provide significant cost advantages, sometimes 30-50% lower than domestic equivalents for comparable quality. The trade-off involves longer lead times, potential communication barriers, and increased logistics complexity.
Here's a comprehensive comparison to guide your decision:
| Factor | Domestic Sourcing | International Sourcing | Factory-Direct International |
|---|---|---|---|
| Typical Lead Times | 2-4 weeks for stock; 6-8 weeks for custom | 6-10 weeks including shipping | 4-8 weeks with integrated operations |
| Communication | Same timezone, native language | Timezone gaps, potential language barriers | Dedicated English-speaking technical teams |
| Pricing | Higher unit costs; lower shipping | Lower unit costs; higher shipping and duties | Factory-direct pricing without middlemen |
| Quality Oversight | Easy facility visits and audits | Requires travel or third-party inspection | Established certifications with virtual tours |
| Minimum Order Quantities | Often higher due to setup costs | Varies widely by supplier | Flexible MOQs with volume incentives |
| Secondary Processing | May require additional vendors | Inconsistent availability | Integrated CNC, finishing under one roof |
The "right" choice depends on your specific situation. High-mix, low-volume projects with tight deadlines often favor domestic partners. High-volume production runs where cost competitiveness drives profitability lean toward international options. Many successful procurement strategies combine both, using domestic suppliers for prototypes and urgent needs while partnering with international custom aluminum extruders for production volumes.
Here's where the sourcing conversation gets interesting. Factory-direct partnerships with established international manufacturers eliminate the middlemen that inflate traditional import pricing. You're working directly with the facility that operates the extrusion presses, runs the CNC machining centers, and manages the finishing lines.
Consider what this means practically. When you source through a domestic distributor who imports profiles, you're paying for their markup, their warehousing, and their overhead. When you partner directly with a manufacturer, those intermediary costs disappear from your supply chain.
Full-service international manufacturers with comprehensive capabilities exemplify this model. For instance, Shengxin Aluminium operates 35 extrusion presses ranging from 600T to 5500T, backed by over 30 years of industry experience. This scale enables factory-direct pricing that distributors simply cannot match while maintaining quality certifications that satisfy demanding applications.
According to full-service fabrication research, working with a single partner who handles everything from raw material to finished component eliminates coordination delays and reduces total project cost. When die development, extrusion, deep processing, and surface treatment happen under one roof, information flows smoothly and accountability remains clear.
The advantages of factory-direct partnerships extend beyond pricing:
For buyers seeking certified aluminum suppliers for custom products, factory-direct relationships also provide traceability advantages. You know exactly where your profiles are manufactured, what quality systems govern production, and who to contact when questions arise.
The best aluminum extrusion partnerships aren't transactional; they're strategic relationships that deliver increasing value over time. Whether you choose domestic, international, or factory-direct sourcing, how you build and maintain vendor relationships determines long-term success.
As partnership research emphasizes, a full-service fabrication partner becomes part of your team. They learn your preferences, understand your business, and work alongside you over the long term. Many successful manufacturing relationships span decades because both parties invest in building trust and mutual understanding.
Consider these relationship-building strategies:
When evaluating potential long-term partners, assess their willingness to invest in the relationship. Vendors who offer design support during quoting, proactively suggest cost-saving modifications, and maintain transparent communication about challenges demonstrate partnership mindset. Those focused solely on order processing typically remain transactional regardless of volume.
The end-to-end support model particularly suits complex projects. When a single vendor handles die development, extrusion production, secondary machining, and surface finishing, project coordination simplifies dramatically. Rather than managing multiple suppliers with different timelines and quality standards, you work with one partner who owns the entire process from concept to delivery.
For buyers ready to explore factory-direct international sourcing, manufacturers like Shengxin Aluminium demonstrate what comprehensive capabilities look like in practice. Their integrated extrusion and deep processing services encompass everything from custom die design through precision CNC machining and advanced surface treatments, providing the single-source partnership that complex projects demand.
With your sourcing strategy defined, the next consideration involves matching vendor capabilities to your specific industry requirements, because different applications demand different vendor strengths.
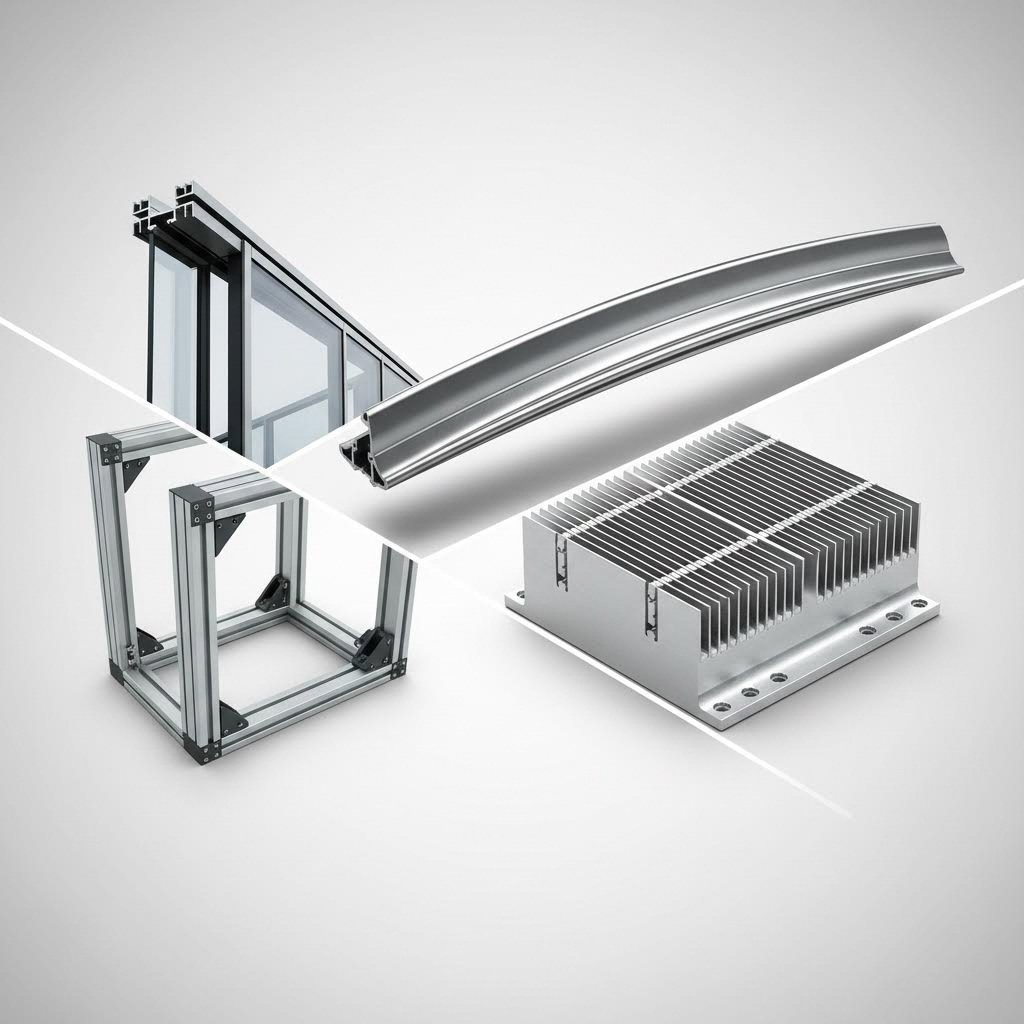
You've evaluated sourcing models and understand the trade-offs between domestic and international partnerships. But here's what separates strategic vendor selection from generic procurement: different industries demand fundamentally different vendor capabilities. The aluminum extrusion rail system perfect for your warehouse automation project requires entirely different expertise than the curved aluminum extrusion gracing an architectural facade. Understanding these distinctions helps you identify vendors who speak your industry's language.
When your project involves buildings, the stakes extend beyond functionality to aesthetics, safety codes, and decades of expected service life. Architectural aluminum extrusion vendors must demonstrate expertise that general-purpose suppliers simply don't possess.
According to industry certification standards, architectural aluminum extrusion profiles require CE certification to ensure the highest standards of safety and performance. This certification matters because building components face rigorous testing requirements that industrial profiles may never encounter.
Consider these factors when evaluating vendors for architectural applications:
The best architectural vendors understand that your aluminum extrusion tube for a handrail system must meet specific deflection requirements under load, while your decorative fascia profiles prioritize visual consistency across an entire building facade. They'll ask about your project's exposure conditions, expected finish longevity, and applicable standards before quoting.
Sounds different from architecture? It absolutely is. Industrial applications prioritize precision, repeatability, and integration with automated systems over aesthetic considerations. Your modular aluminum framing for a production line must maintain dimensional accuracy that enables components to assemble predictably across thousands of units.
According to industrial automation research, aluminum structural framing serves as the literal foundation and framework for many industrial automation tasks. Application areas include autonomous mobile robots, collaborative robots, conveyance technology, machine guarding, material flow systems, and workstations.
When evaluating vendors for industrial and automation needs, prioritize these capabilities:
The flexibility of small aluminum extrusions for automation framing allows reconfiguration as production needs evolve. Vendors experienced in this sector understand that your initial design will likely change, and they'll help you select profile systems that accommodate future modifications without requiring entirely new tooling.
What happens when your application doesn't fit neatly into architectural or industrial categories? Specialty applications demand vendors with specific technical knowledge and often require custom tooling that pushes standard extrusion capabilities.
These specialty categories each carry unique requirements:
For applications requiring curved aluminum extrusion, verify that vendors operate CNC bending equipment capable of achieving your radius specifications without compromising profile integrity. Not all suppliers can bend extruded profiles, and those who do vary significantly in minimum bend radius capabilities and surface finish preservation.
The key insight across all specialty applications is this: vendors experienced in your specific industry understand the standards, testing requirements, and performance expectations without requiring extensive education from you. They've solved similar problems before and can anticipate challenges that generalist suppliers might miss entirely.
When requesting quotes, explicitly state your application context. A vendor who asks follow-up questions about operating environment, performance requirements, and applicable standards demonstrates the industry knowledge that translates to successful project execution. Those who quote based solely on profile geometry, without understanding your end-use, may deliver technically compliant parts that fail in actual application.
With industry-specific considerations understood, you're ready to synthesize everything learned into a practical action plan that transforms your vendor search into lasting partnerships.
You've learned how to evaluate technical capabilities, compare sourcing models, and match vendors to your industry requirements. Now it's time to transform that knowledge into decisive action. The difference between buyers who build exceptional supply chains and those who struggle with vendor problems often comes down to execution. Here's your roadmap for moving from evaluation to partnership.
Feeling overwhelmed by everything you've learned? Don't worry. Use this consolidated checklist to guide your aluminium extrusion vendor evaluation systematically:
According to procurement best practices, starting with smaller orders to test vendor performance before committing to large volumes reduces risk significantly. A trial run reveals how vendors handle real production challenges, not just how they respond to RFQs.
Where to buy aluminum extrusion is only the first question. How you maintain that relationship determines whether you're building a strategic partnership or just processing transactions.
As supplier relationship research emphasizes, effective SRM goes beyond transactional procurement to ensure suppliers align with your organization's strategic goals. The same principles apply to your custom aluminum products sourcing:
For buyers seeking top aluminum suppliers for custom products with bespoke aluminium extrusion capabilities, established manufacturers provide significant advantages. Companies like Shengxin Aluminium offer technical support from initial design through mass production, combining 30+ years of experience with comprehensive deep processing services that simplify complex projects.
Should you rely on a single vendor or spread your sourcing across multiple partners? According to supply chain diversification guidance, having backup suppliers of different sizes, in different locations, and with different capabilities ensures you don't completely rely on one source for business-critical materials.
Consider diversifying your vendor base when:
Your vendor search doesn't end with the first successful order. Continuously evaluate performance, explore emerging suppliers, and refine your partnerships based on real-world results. The aluminum extrusion vendors who earn your long-term business will be those who consistently deliver quality, communicate transparently, and adapt as your requirements evolve.
Manufacturers operate extrusion presses and control the entire production process from billet heating to surface treatment, investing in equipment, finishing workshops, and quality systems. Distributors purchase profiles from manufacturers and provide value-added services like cutting, machining, and assembly. Manufacturers excel at custom extrusions and large-volume orders with minimum quantities, while distributors maintain stock for smaller orders with quicker turnaround on standard shapes.
Lead times vary based on project complexity. Die manufacturing typically takes 10-20 days, extrusion production requires 7-15 days, and surface finishing adds 5-10 days. Total project timelines range from 4-6 weeks for standard projects. Complex designs requiring fabrication and anodizing may need 16-20 weeks. Vendors with integrated operations handling extrusion, machining, and finishing under one roof typically deliver shorter, more predictable lead times.
A comprehensive RFQ should include technical drawings in CAD formats (STEP, IGES, DXF), quantity requirements with annual projections, tolerance specifications highlighting critical dimensions, finish requirements with color codes and standards, delivery timelines, quality certifications needed, and secondary processing requirements. Including alloy and temper specifications, application context, inspection expectations, and packaging requirements helps vendors provide accurate, comparable quotes.
Factory-direct partnerships eliminate middleman markups, warehousing costs, and distributor overhead from your supply chain. Working directly with manufacturers like Shengxin Aluminium provides access to 35 extrusion presses, comprehensive deep processing services, and technical support from design through production. Additional benefits include streamlined project management, flexible finishing options, integrated CNC machining, and consistent quality control under unified standards.
Assess vendors based on press tonnage range, maximum profile dimensions, tolerance capabilities meeting Aluminum Association standards, and secondary processing options. Request ISO 9001 certification at minimum, plus industry-specific certifications for specialized applications. Evaluate their die development expertise, CNC machining precision, in-house finishing capabilities, and ask for first-article inspection reports and capability studies from similar projects.


 un service en ligne
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 français
 English
 Deutsch
 русский
 español
 português
 العربية
 ไทย
 Việt
 Українська