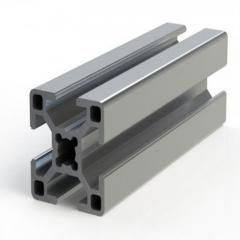
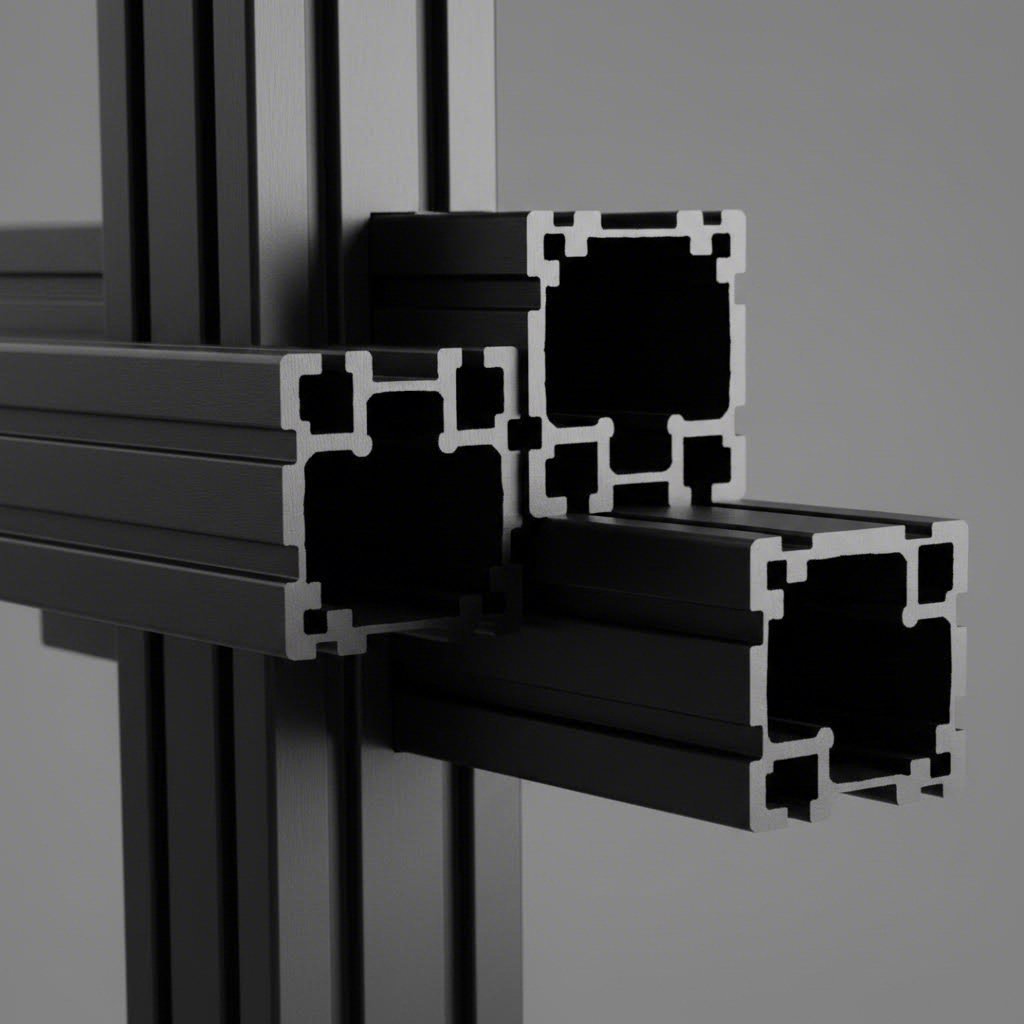
Have you ever wondered what gives those sleek, dark aluminum frames their striking appearance? When you see industrial equipment, modern furniture, or precision 3D printer enclosures with that distinctive dark finish, you're likely looking at black aluminum extrusion. But here's the thing—aluminum doesn't naturally come in black. So what makes these profiles different from the standard silver versions you might be more familiar with?
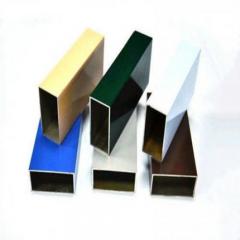
Black aluminum extrusion refers to extruded aluminum profiles that have undergone specialized surface treatment processes to achieve their dark finish. Unlike raw mill-finish aluminum, which has a dull, matte appearance with visible marks or scratches, these treated profiles feature a protective and aesthetically pleasing black coating. The two primary methods for achieving this finish are black anodizing and powder coating—each offering distinct advantages depending on your application needs.
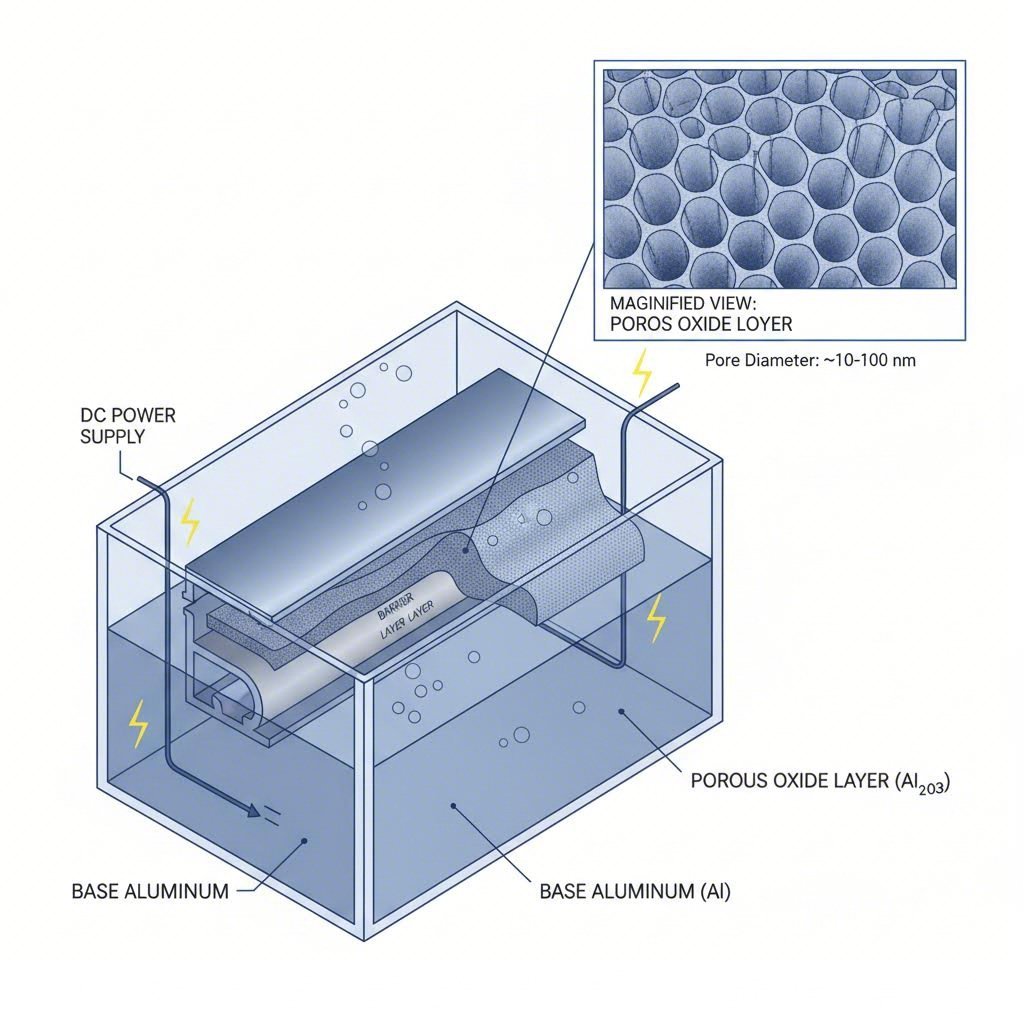
The transformation from standard silver to deep black happens through electrochemical or thermal processes applied after the aluminum is forced through a shaped die. During anodizing, an electrochemical reaction builds a thick, protective oxide layer on the aluminum surface. This porous layer then absorbs black dye before being sealed, locking in both color and protection. The result? A finish that's integral to the metal itself—meaning it won't peel or flake like traditional paint.
Powder coating takes a different approach. A dry powder is applied electrostatically to the aluminum surface, then cured under heat to form a durable coating. While this method sits on top of the aluminum rather than becoming part of it, it offers excellent color consistency and flexibility for various applications.
Why are designers, engineers, and hobbyists increasingly choosing anodized aluminum over standard mill-finish profiles? The answer lies in performance combined with aesthetics. Mill-finish aluminum features only a thin natural oxide layer that offers minimal protection against corrosion and environmental wear. In contrast, black anodized surfaces provide significantly enhanced durability.
Here are the primary characteristics that make black aluminum extrusion stand out:
From automation equipment and 3D printer enclosures to modular workstations and architectural elements, these profiles have become the go-to choice when both performance and visual appeal matter. Industries including robotics, aerospace, retail, and entertainment now regularly specify black finishes for their aluminum framework needs. As you explore the different series options and finishing methods in the sections ahead, you'll discover exactly how to match the right profile to your specific project requirements.
So you've decided you want black extruded aluminum for your project—but should you choose anodized or powder coated? Understanding how each process works will help you make the right decision. Let's break down the science behind these finishing methods so you can confidently select the option that matches your application requirements.
Imagine transforming the surface of aluminum at a molecular level. That's essentially what happens during anodizing—a sophisticated electrochemical process that's been refined over the past century to deliver exceptional results.
The journey to creating anodized aluminum extrusions begins with thorough preparation. The aluminum profile first undergoes extensive cleaning and degreasing to eliminate any surface contaminants that could disrupt the final finish. Even microscopic particles can affect the uniformity of the oxide layer, so this step is critical.
Once prepared, the aluminum enters an acid electrolyte bath—typically sulfuric acid—where precise electrical current is applied. Here's where the magic happens: the controlled electrical stimulation drives aluminum atoms to combine with oxygen, forming aluminum oxide directly on the profile's surface. This oxide layer isn't just sitting on top of the metal; it's growing from the base aluminum, making it an integral part of the structure that cannot peel or flake.
The resulting oxide layer has a unique porous structure, almost like a honeycomb at the microscopic level. This porosity is essential for achieving the black color. Black dye molecules are absorbed into these tiny pores, penetrating deep into the oxide layer. The final step involves sealing the pores—typically through hot water or steam treatment—which locks in the dye and creates a smooth, protected surface.
For anodized extruded aluminum profiles with 20mm slot widths or similar dimensions, the coating thickness directly correlates with durability. Class I architectural anodizing achieves approximately 0.7 mils (about 18 microns) thickness, while Class II provides around 0.4 mils. The thicker the coating, the longer it lasts—and the more vibrant the color retention over time.
While anodizing transforms the aluminum surface itself, powder coating takes a fundamentally different approach. Think of it as applying a protective shell rather than modifying the core material.
Powder coating uses finely ground particles of pigment and resin that carry an electrostatic charge. When sprayed onto the grounded aluminum profile, these particles cling to the surface uniformly. The coated piece then enters a curing oven where temperatures typically reach 350-400°F (175-200°C), causing the powder to melt and flow together into a continuous, durable film.
One significant advantage of powder coating? It produces zero volatile organic compounds (VOCs) during application, and overspray can be collected and recycled. This makes it an environmentally friendly option that many manufacturers appreciate. Plus, powder coatings can achieve thicker layers than traditional paints—often 2-4 mils—providing robust physical protection.
But here's the key distinction: while powder coating creates an excellent protective barrier, it remains a separate layer on top of the aluminum. Under extreme abrasion or impact, it can potentially chip or separate from the base metal. Anodized finishes, being integral to the aluminum, won't chip in the same way—though they can wear through under severe conditions.
What about traditional painting? Liquid paint involves pigment, resin, and solvents that evaporate during curing. While paint offers the most extensive color matching capabilities and is easy to apply in small batches, it typically provides less durability than either anodizing or powder coating for aluminum extrusions in demanding applications.
| Criteria | Black Anodized Aluminum | Powder Coated Black | Painted Aluminum |
|---|---|---|---|
| Durability | Excellent—integral to metal surface | Very Good—robust protective layer | Moderate—susceptible to chipping |
| Scratch Resistance | High—hardened oxide surface | Good—can chip under heavy impact | Lower—scratches more easily |
| UV Stability | Excellent—minimal fading | Good to Excellent (PVDF resins best) | Variable—depends on paint quality |
| Coating Thickness | 0.4–0.7 mils (10–18 microns) | 2–4 mils (50–100 microns) | 1–2 mils (25–50 microns) |
| Corrosion Resistance | Excellent when properly sealed | Very Good—thicker barrier layer | Good—requires proper pretreatment |
| Color Options | Limited—primarily metallic tones | Extensive—hundreds of colors/textures | Unlimited—custom matching available |
| Cost Considerations | Moderate—process-intensive | Moderate—efficient for large batches | Lower initial—higher maintenance |
| Renewability | Can be cleaned to restore appearance | Requires recoating if damaged | Requires repainting if damaged |
One often-overlooked advantage of anodized aluminum extrusions? Their renewability. According to industry specialists at SAF, anodized surfaces that appear worn can often be restored through proper cleaning with mild detergent and abrasive techniques—a small amount of the oxide layer is removed, revealing a renewed finish beneath. Once paint or powder coating fails, however, complete recoating becomes the only option.
When selecting between these finishes, consider your priorities. Need maximum abrasion resistance for high-traffic areas? Anodizing excels. Want a specific color with excellent impact protection? Powder coating delivers. Working with tight budgets on interior applications? Quality paint may suffice. Understanding these distinctions ensures your black aluminum profiles perform exactly as your project demands—which brings us to an equally important decision: selecting the right profile series for your structural requirements.
You've chosen your finish—now comes the question that trips up even experienced builders: which series size do you actually need? If you've browsed aluminum extrusion catalogs, you've probably encountered numbers like 1515, 2020, 3030, 4040, and 8020 without any clear explanation of what they mean. Let's demystify this numbering system so you can confidently match profiles to your project requirements.
Here's the simple truth that manufacturers rarely explain upfront: series numbers directly correspond to the profile's cross-sectional dimensions in millimeters. A 2020 profile measures 20mm x 20mm. A 4040 profile? That's 40mm x 40mm. And when you see asymmetrical numbers like 20 x 40 or 40 x 20, you're looking at rectangular profiles where one dimension differs from the other—perfect for situations requiring greater strength in one direction.
But the series designation tells you more than just size. It also determines the T-slot width, which directly affects hardware compatibility. According to industry specifications from Bitfab, each profile series has distinct slot and threaded hole measurements that dictate which fasteners will work:
Why does this matter? Imagine building a frame with 1515 aluminum extrusion profiles but accidentally ordering M8 T-nuts designed for 4040 series. They simply won't fit. Understanding series compatibility from the start saves you from frustrating—and costly—mistakes.
Selecting the right series isn't just about physical dimensions—it's about matching structural capability to your actual requirements. Each jump in series size delivers significantly greater stiffness and load capacity, but also adds weight and cost. Here's how different series align with common applications:
What about rectangular profiles? Options like 20 x 40 and 40 x 20 provide directional strength advantages. A 20 x 40 profile oriented with the 40mm dimension vertical offers greater resistance to bending in that plane—useful for uprights in frame designs. Flip it to 40 x 20 orientation, and you've got a low-profile horizontal member with enhanced lateral stiffness.
Here's where global projects get interesting. While metric sizing dominates most of the world, North American manufacturers often offer imperial equivalents. A 1-inch series profile roughly corresponds to 25mm metric, while 1.5-inch profiles approximate 40mm series in capability.
Which system should you choose? Consider these factors:
Perhaps the most critical factor in series selection involves understanding how profiles perform under load. According to technical data from Raptor Supplies, load capacity varies dramatically between series—and the relationship isn't linear.
A 40 series profile doesn't simply handle twice the load of a 20 series; it often supports four to six times more weight due to the exponential relationship between cross-sectional area and moment of inertia. When calculating your requirements, consider:
When in doubt, size up. The cost difference between a 3030 and 4040 profile is minimal compared to the expense of rebuilding an undersized frame that flexes or fails under real-world conditions.
Now that you understand how series numbers translate to performance capability, let's explore how the T-slot design enables the modular assembly that makes these profiles so versatile.
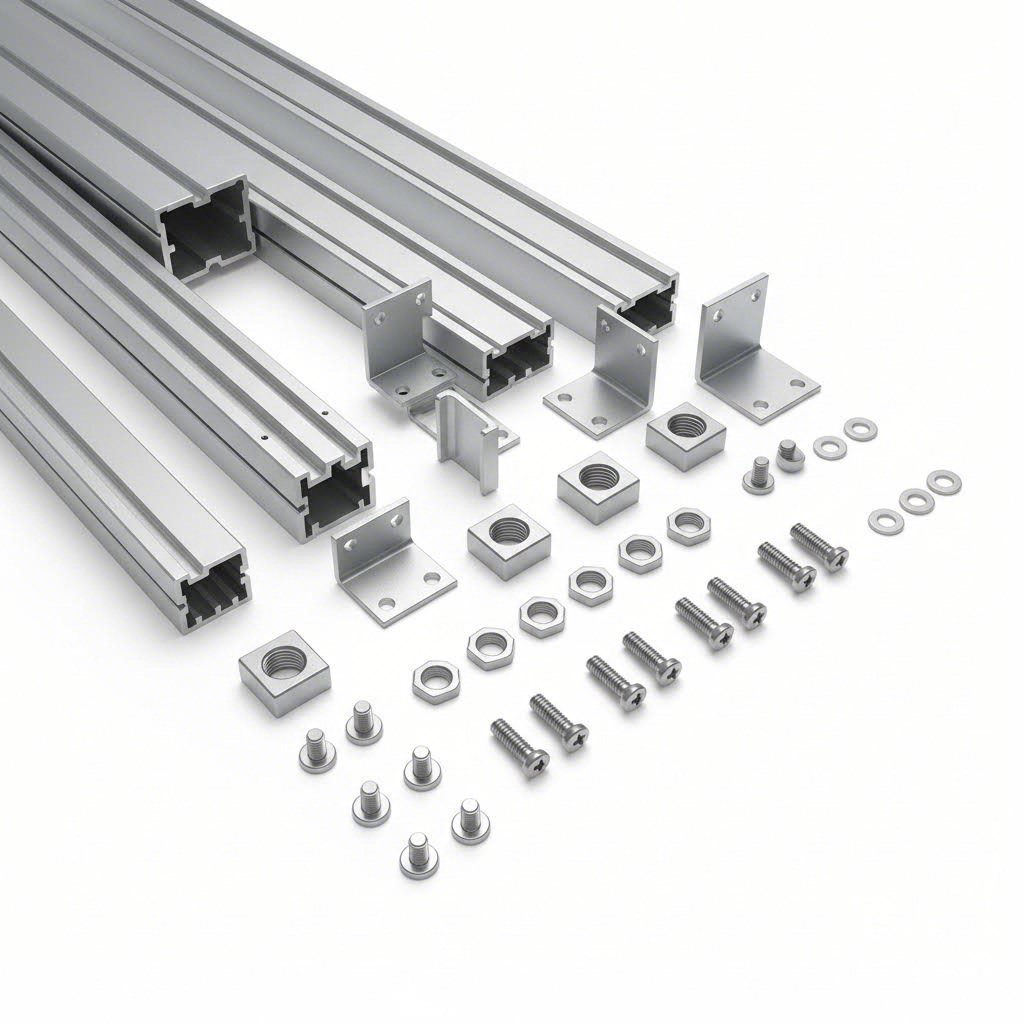
Ever looked at a modular aluminum frame and wondered how everything stays together without visible welds or permanent fasteners? The secret lies in the ingenious T-slot design that runs along each face of these profiles. Understanding how this system works—and which connectors to use—transforms you from a confused catalog browser into a confident builder ready to tackle any project.
Picture this: a channel shaped like the letter "T" running the entire length of your aluminum extrusion profile. This seemingly simple feature is what makes modular framing systems revolutionary. The T-shaped groove accepts specialized hardware that slides into position, locks in place, and creates secure connections at any point along the profile—not just at predetermined holes or fixed intervals.
Here's why this matters for your projects. Traditional metal framing requires drilling, welding, or using pre-punched holes that limit your design options. With a t slot aluminum profile, you gain complete freedom to position connections exactly where structural requirements or design aesthetics demand. Need to shift a bracket three inches to the left? Simply loosen, slide, and retighten—no new holes required.
The beauty of this system extends to black aluminum extrusion as well. Whether you're working with anodized or powder coated profiles, the T-slot dimensions and functionality remain identical to standard silver finishes. Your 80/20 aluminum connectors work seamlessly regardless of color, meaning you can mix aesthetic choices without worrying about hardware compatibility. The only difference is appearance—the underlying engineering stays exactly the same.
Think of the T-slot as a universal mounting rail built into every face of your profile. This means a single piece of 4040 extrusion offers four independent mounting channels, while rectangular profiles like 20x40 or 40x80 provide even more connection options. The possibilities multiply quickly when you start combining profiles into complex assemblies.
Now that you understand the T-slot concept, let's explore the hardware that makes it all work. According to detailed documentation from Phidgets, several connector categories serve different structural purposes—and choosing the right ones determines whether your frame stands solid or wobbles under load.
T-nuts are the workhorses of any T-slot assembly. These small but critical components slide into the channel and provide threading for bolts that secure brackets, panels, and accessories. But not all T-nuts are created equal:
Matching nut size to your profile series is non-negotiable. A v slotted aluminum insert designed for 20 series slots simply won't fit 40 series channels—the dimensions differ significantly. Always verify compatibility before ordering hardware.
Creating right-angle connections requires brackets engineered for the T-slot ecosystem. Industry experts at A-Line Automation categorize these into several types:
For structural applications similar to 4x4 post brackets used in wood construction, the diecast aluminum corner brackets provide comparable rigidity. Much like a 4x4 post base anchors wooden columns, heavy-duty anchor connectors secure aluminum profiles to floors or existing structures. And just as you'd select appropriate bolts for 4x4 posts based on load requirements, choosing the right T-slot fastener size ensures your connections handle real-world forces.
Ready to build? Following a systematic approach prevents frustration and ensures structural integrity. Here's the proven sequence that experienced 80 20 aluminum fabricators follow:
The T-slot system's versatility extends far beyond structural joints. According to accessory specialists at Parco, dozens of add-on components transform basic frames into complete functional assemblies:
The key advantage here? Every accessory mounts using the same T-nut and bolt system you're already using for structural connections. No special tools, no proprietary fasteners—just consistent, modular hardware throughout your entire project.
With your understanding of T-slot mechanics and connector options now solid, you're ready to explore where black aluminum extrusion truly shines—the specific applications where that dark finish delivers advantages beyond mere aesthetics.
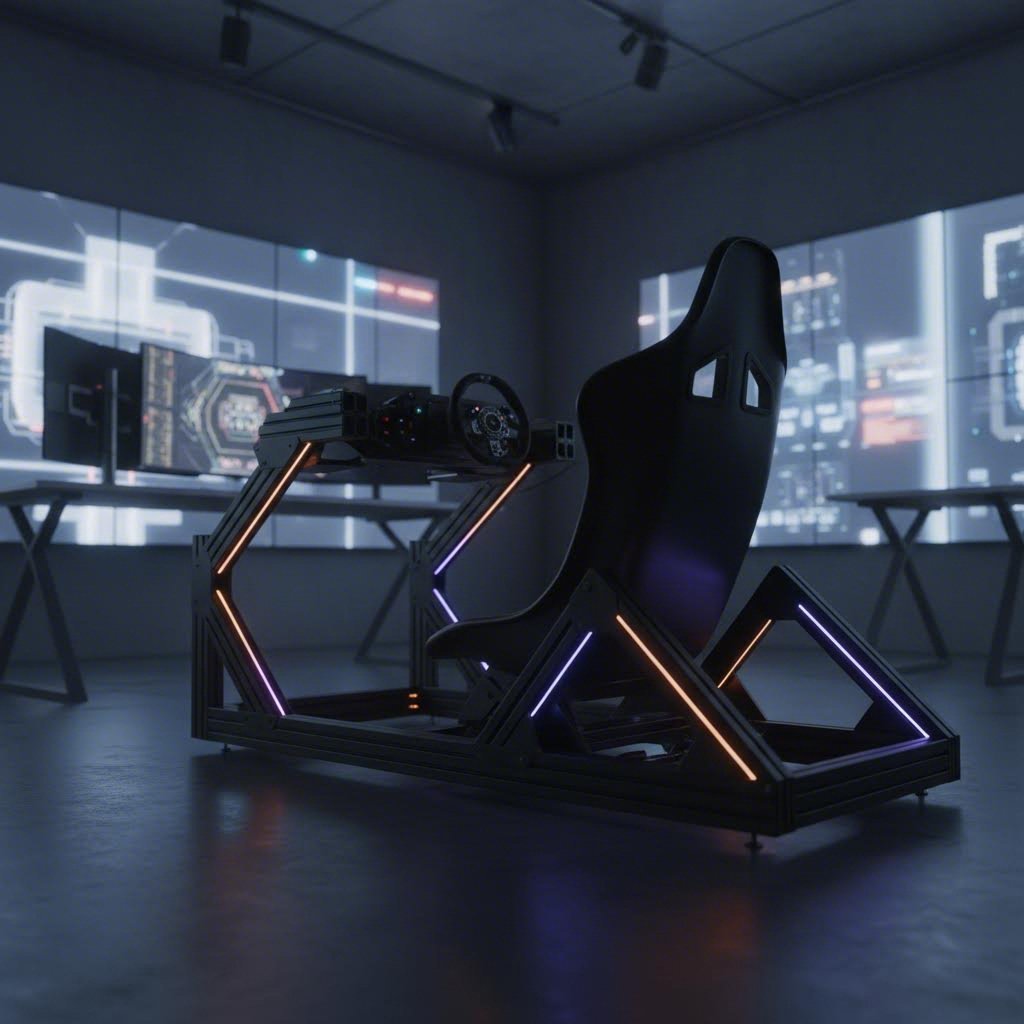
Now that you understand the mechanics of T-slot assembly, let's answer the question every builder eventually asks: when does choosing black aluminum over standard silver finishes actually matter? Spoiler alert—it's about far more than just looking cool. From functional advantages in specific environments to practical benefits that reduce maintenance headaches, these dark profiles deliver tangible value across surprisingly diverse applications.
Picture a photography studio with bright lights bouncing everywhere. Now imagine a silver aluminum frame reflecting those lights directly into your camera lens. Frustrating, right? This is exactly why black aluminum frame construction dominates creative industries where light control matters.
The practical benefits of dark finishes extend well beyond aesthetics:
When you're building a 2x3 frame for a compact display or a larger 4x4 picture frame for gallery installations, the finish choice directly impacts both functionality and visual impact. Black aluminum tubing and profiles create cohesive visual statements that silver simply cannot match in design-forward applications.
Let's break down where these profiles truly shine, organized by the industries that rely on them most heavily:
Want to see these principles in action? The sim racing community has embraced black aluminum extrusion with particular enthusiasm, and for good reason.
According to one experienced builder's detailed account, constructing a custom rig using 40-series aluminum extrusions delivers unmatched rigidity for high-end direct drive wheel systems—the force feedback from these advanced bases demands frames that won't flex or vibrate. While the materials alone for a DIY extrusion rig can exceed $600 before hardware costs, the full adjustability and aesthetic integration with gaming equipment justify the investment for serious enthusiasts.
Key considerations for sim racing applications include:
The builder's advice? Unless you genuinely enjoy designing from scratch, consider pre-engineered chassis options from manufacturers like Trak Racer—they deliver similar rigidity and aesthetics without the complexity of full custom CAD design.
Whether you're building a sim racing cockpit, framing retail displays, or constructing laboratory equipment, understanding the technical specifications behind your black profiles ensures optimal performance. Let's examine the standards and ratings that separate quality finishes from inferior alternatives.
You've seen the filter options on supplier websites—coating thickness, hardness ratings, corrosion resistance classes—but what do these specifications actually mean for your project? When comparing black aluminum extrusion products across manufacturers, understanding these technical standards separates informed purchasing decisions from expensive guesswork. Let's decode the numbers so you can confidently evaluate quality.
When manufacturers reference coating specifications, they're typically following standards established by military and industry organizations. The most widely recognized benchmark is MIL-A-8625, a military specification that defines anodic coating types, thicknesses, and performance requirements for aluminum and aluminum alloys.
Here's what you need to know about the coating classifications you'll encounter:
The class designation matters equally. Class 1 indicates non-dyed coatings, while Class 2 specifies dyed finishes—including black. According to the Aluminum Anodizers Council, black coloring for Class 2 finishes can be achieved through organic dyes, inorganic compounds, or electrolytic deposition of metallic salts like tin, cobalt, or nickel into the porous oxide layer.
Why does coating thickness matter so much? Thicker oxide layers provide greater durability, better dye absorption for richer color, and enhanced corrosion protection. For architectural applications, industry standards specify Class I finishes at approximately 0.7 mils (18 microns) minimum thickness, while Class II finishes require roughly 0.4 mils (10 microns). When evaluating supplier specifications, verify which class standard they're referencing—the performance difference is substantial.
Beyond thickness, several performance metrics determine how well your black aluminum profiles will hold up under real-world conditions. Understanding these ratings helps you match specifications to application demands—whether you're building interior equipment frames or outdoor architectural elements.
Standard Type II anodized coatings provide good surface hardness suitable for most commercial and industrial applications. However, when extreme wear resistance is required, Type III hard anodizing delivers exceptional performance. According to MIL-A-8625 specifications, hard anodized coatings achieve Rockwell C hardness ratings between 50 and 70—described as "file hard" in industry terminology.
For Type III coatings, the specification requires a maximum wear index of 1.5mg per 1000 cycles for most alloys (3.5mg/1000 cycles for high-copper alloys like 2024) when tested using the CS-17 abrasion wheel method. These coatings excel in sliding applications, valve components, and machine parts subjected to repeated contact.
One important consideration: sealing Type III coatings—which enhances corrosion resistance—actually reduces abrasion resistance. If wear protection is your primary concern, unsealed hard anodizing may be the better choice despite marginally lower corrosion performance.
The standard benchmark for corrosion performance is salt spray testing per ASTM B 117. Properly anodized and sealed aluminum must withstand 336 hours of continuous salt fog exposure with no more than 15 isolated pits across 150 square inches of test area—and no single pit larger than 0.031 inch diameter.
For outdoor installations, this testing correlates to real-world durability. Profiles meeting these requirements handle coastal environments, industrial atmospheres, and weather exposure without significant degradation. When reviewing manufacturer data, look for explicit reference to salt spray hours and compliance with MIL-A-8625 or equivalent commercial standards.
Outdoor applications demand finishes that won't fade under sunlight exposure. The light fastness standard for dyed anodic coatings requires a Delta E value of 3 or less after 200 hours of accelerated UV exposure testing per ASTM G 23 or ASTM G 26 methods.
What does Delta E mean practically? It's a measure of color difference—values below 3 are generally imperceptible to the human eye. Black finishes typically perform well in UV resistance because the dyes used (often metal-salt based rather than organic) demonstrate inherent stability. However, organic dyes in other colors may fade more readily, which is why black remains a popular choice for exterior applications.
According to anodizing industry guidance, electrolytically deposited colors using tin, cobalt, or nickel salts offer superior colorfastness compared to organic dyes—an important distinction when specifying finishes for long-term outdoor installations.
| Specification | Type II (Standard) | Type III (Hard Coat) | Powder Coating |
|---|---|---|---|
| Typical Thickness | 0.4–1.0 mils (10–25 microns) | 0.5–4.5 mils (13–114 microns) | 2–4 mils (50–100 microns) |
| Hardness Rating | Moderate (200–400 HV) | High (Rockwell C 50–70) | Lower than anodized |
| UV Stability | Excellent (ΔE <3 at 200hrs) | Excellent | Good to Excellent (PVDF best) |
| Salt Spray Resistance | 336+ hours (sealed) | 336+ hours (when sealed) | 500–1000+ hours |
| Recommended Applications | General industrial, architectural, consumer products | High-wear components, machinery, aerospace | Architectural, outdoor furniture, appliances |
When your project demands tight fits—think precision assemblies, automation equipment, or applications with specific metal stud dimensions requirements—understanding how anodizing affects part dimensions becomes critical.
Here's what happens during the anodizing process: approximately half the coating thickness grows outward from the original aluminum surface, while the other half penetrates inward. For a 2-mil Type III coating, expect roughly 1 mil (0.001 inch) of dimensional growth per surface. This means a shaft anodized on all sides increases in diameter by approximately 2 mils total.
According to MIL-A-8625 specifications, coating thickness tolerances for Type III coatings must remain within ±20% for coatings up to 2 mils, and ±0.4 mils for thicker applications. When specifying parts for precision fits, provide both machining dimensions and final coated dimensions on your drawings—experienced anodizers can achieve tolerances as tight as ±0.0001 inch with careful process control.
For threaded components, the dimensional impact compounds. External thread major and minor diameters increase by twice the growth amount, while 60-degree thread pitch diameters increase by four times the growth. If your design includes threaded holes or fastening points, account for these changes during the machining phase or specify post-anodizing thread tapping.
When designing frames where stud spacing and alignment matter—similar to construction applications with precise metal stud dimensions—request tolerance data from your supplier upfront. Reputable manufacturers provide dimensional certificates confirming their process capabilities match your requirements.
When comparing products across suppliers, focus on these key data points:
Quality manufacturers willingly provide test certificates and detailed specification data. If a supplier hesitates or offers only marketing language instead of technical data, consider that a warning sign about their process control and quality assurance practices.
With these specifications in hand, you're equipped to evaluate black aluminum profiles objectively. But what happens when you need to cut, drill, or machine these finished profiles without damaging that carefully applied coating? The next section addresses fabrication techniques that protect your investment in quality finishes.
You've selected the perfect black aluminum extrusion for your project, verified the specifications, and planned your frame design. Now comes the moment of truth—cutting and machining those beautiful profiles without ruining the finish you paid extra to obtain. Here's the reality: that anodized coating is remarkably hard, which makes it both durable in use and challenging to machine cleanly. Understanding how to cut extruded aluminum properly protects your investment and ensures professional-looking results.
Imagine spending hours assembling a pristine frame only to notice ugly chips and scratches around every cut end. This happens more often than you'd think—and it's almost always preventable with proper technique and tooling.
The anodized layer on black aluminum profiles is significantly harder than the base aluminum beneath it. According to machining specialists at Sunrise Metal, this hardness difference means cutting tools wear faster on anodized material than on untreated aluminum. More critically, improper cutting techniques cause the brittle oxide layer to chip, crack, or flake—leaving unsightly damage that's impossible to repair without refinishing.
Three primary cutting methods work well for black aluminum extrusion, each suited to different situations:
Regardless of which cutting method you choose, following these proven techniques dramatically improves results:
Cutting is straightforward compared to drilling, tapping, and milling operations where tooling directly contacts the finished surface. The key challenge? Preventing finish damage around machined features while achieving accurate dimensions.
Sharp tooling is non-negotiable when working with anodized aluminum. Dull drill bits grab and tear rather than cutting cleanly, causing the hard oxide layer to chip around hole edges. According to industry guidance, carbide cutting tools remain the best choice for anodized material because they maintain sharp edges longer than high-speed steel alternatives. High-helix carbide end mills work particularly well for CNC operations.
When drilling, several techniques protect the finish:
For tapping operations, the approach changes slightly. Thread-forming taps (rather than thread-cutting taps) work well for softer aluminum alloys because they displace material rather than removing it. However, the hardened anodized surface may require thread-cutting taps to avoid cracking the oxide layer. When threading holes for applications similar to screws for metal studs, using the correct tap style for anodized material prevents the frustrating experience of chipped threads that won't accept fasteners properly.
Here's a decision that impacts both quality and cost: should you order profiles pre-cut to length or cut them yourself? The answer depends on your project scale, equipment access, and tolerance requirements.
Order pre-cut lengths when:
Cut on-site when:
Some projects demand capabilities beyond basic cutting. Custom machining services—including precision drilling, counter-boring, thread tapping, and complex profile modifications—often deliver better results than DIY approaches, especially for:
Many extrusion suppliers offer integrated machining services, processing profiles immediately after cutting while they're still fixtured. This approach ensures dimensional accuracy and eliminates shipping damage risks associated with sending finished profiles to separate machine shops.
The investment in proper cutting and machining techniques—or the wisdom to outsource operations beyond your capabilities—pays dividends throughout your project's lifespan. Clean cuts and precise holes mean easier assembly, better aesthetics, and frames that perform exactly as designed. With fabrication fundamentals covered, the next consideration is maintaining that pristine black finish over months and years of use.
You've invested in quality black aluminum extrusion, cut it precisely, and assembled a beautiful frame. Now what? Here's the good news: anodized surfaces are remarkably low-maintenance compared to painted or powder coated alternatives. But "low-maintenance" doesn't mean "no maintenance." Proper care extends the life of your black aluminium extrusion and keeps it looking professional for years—even decades—of service.
Understanding what you're protecting helps explain why certain care approaches work better than others. Remember, the black and aluminum oxide layer isn't sitting on top of the metal—it's an integral part of the surface structure. This means you can't simply strip and reapply the finish like paint. Once damaged, restoration becomes significantly more complex.
According to maintenance specialists at Mid America Specialty Services, oxidation leads to gradual color loss over time as the protective oxide layer deteriorates. Environmental exposure—particularly to masonry materials like lime and concrete, air-borne salts in coastal areas, and harsh weather pollutants—accelerates this process. Proactive cleaning remains your first line of defense against premature wear.
The key principle? Remove environmental contaminants as quickly as possible. Allowing dirt, debris, and chemical residues to accumulate causes the finish to wear away more quickly, shortening asset life and increasing long-term replacement costs. A few minutes of regular maintenance prevents hours of restoration work later.
Routine cleaning couldn't be simpler—but using the wrong products can cause more harm than the dirt you're trying to remove. As noted by Light Metals Coloring's maintenance guide, mild soapy water and a soft cloth are usually sufficient to remove dust, dirt, and smudges from anodized aluminum surfaces.
For lightly soiled profiles, follow this straightforward procedure:
For stubborn stains or accumulated grime, a non-abrasive sponge or soft-bristle brush can be employed with light pressure. Apply uniform pressure using horizontal motions first, then vertical. When grime proves particularly resistant, sponge the surface while simultaneously rinsing to prevent residue buildup.
Regular inspection helps catch problems early. According to industry guidance, surface scratches appear as thin lines or marks on the anodized layer, while dents result from impacts or excessive pressure. Look for areas with pitting, discoloration, or rough texture that might indicate corrosion—particularly in extreme environments or where the anodized layer may be compromised.
For minor surface scratches, you can attempt DIY repair:
When scratches breach the anodized layer entirely, or when damage is extensive, professional refinishing becomes necessary. Trained refinishers can apply clear protective coatings to rejuvenate faded finishes, and high-performance paints can restore the appearance of severely damaged profiles.
Several environmental conditions influence how long your black finishes maintain their appearance:
The most vulnerable time for your black aluminum profiles? During construction and installation, when other trades, debris, and handling create damage risks. Take these precautions:
Investing in preventative care during construction costs far less than restoration work after damage occurs. With proper handling and regular maintenance, your black aluminum extrusion will maintain its professional appearance through years of demanding service—making the next decision equally important: choosing the right supplier who delivers quality worth maintaining.
You've mastered the technical specifications, understand the finishing options, and know exactly which series fits your project. But here's where many buyers stumble: finding a supplier who can actually deliver what you need. Sourcing black aluminum extrusion involves more than comparing unit prices—it requires evaluating manufacturing capabilities, quality systems, and service integration that directly impact your project's success. Let's walk through the evaluation process that separates reliable manufacturing partners from suppliers who leave you scrambling.
Imagine ordering custom profiles only to discover your supplier lacks the press capacity for your profile dimensions, or can't anodize in the black shade you specified. These scenarios happen more often than you'd expect—and they're entirely preventable with proper supplier evaluation.
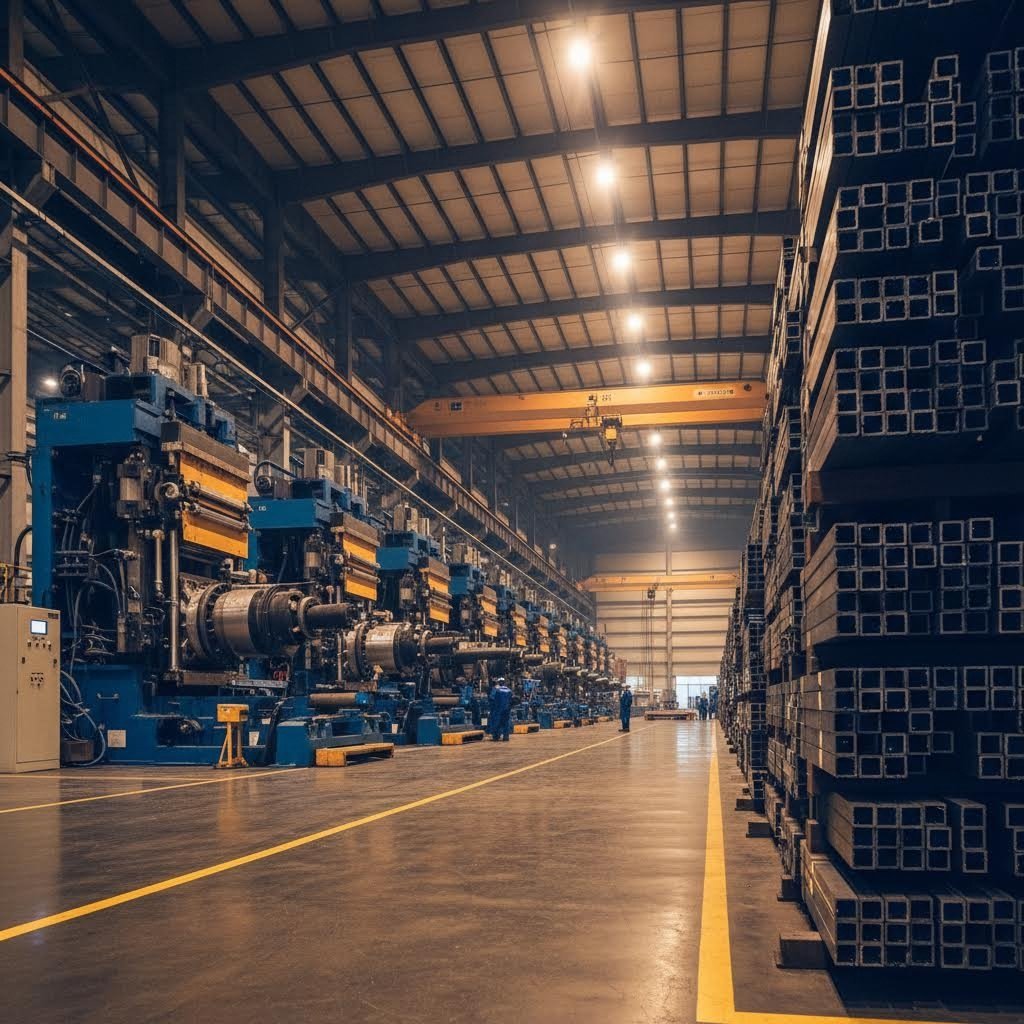
According to industry experts at Aluphant, the extrusion press defines what kind of profiles a supplier can produce. Understanding press capacity ranges helps you match supplier capabilities to your specific requirements:
Why does press range matter beyond simple capability? A supplier operating multiple press capacities can accommodate your projects as they scale—from prototype quantities through production volumes—without requiring you to qualify additional vendors. This flexibility proves invaluable when project requirements evolve mid-stream.
For example, Shengxin Aluminium operates 35 extrusion presses ranging from 600T to 5500T, enabling production of everything from precision small-series profiles to heavy industrial sections within a single manufacturing relationship. This breadth eliminates the common scenario where buyers must coordinate between multiple suppliers for different profile sizes.
Press capacity is just the starting point. A comprehensive evaluation examines the complete manufacturing ecosystem—from raw material handling through finished part delivery. Here's what distinguishes capable suppliers from those likely to create project headaches:
Custom profiles require custom dies—and die quality directly determines profile accuracy, surface finish, and dimensional consistency. According to procurement guidance from Aluphant, many suppliers outsource die manufacturing to third parties, leading to longer lead times and slower problem resolution when issues arise.
Suppliers with in-house die workshops can modify or repair dies quickly, ensuring production continuity. When evaluating potential partners, ask specifically about:
For black aluminum extrusion specifically, surface treatment capability separates suppliers who can deliver from those who must subcontract—adding cost, lead time, and quality control variables. Essential capabilities include:
Shengxin Aluminium exemplifies integrated finishing capability, offering anodizing in custom colors (including champagne and rose gold alongside standard black), powder coating, PVDF, and micro-arc oxidation—all under one roof. This integration ensures batch consistency between dimension and color that becomes impossible to guarantee when profiles travel between separate facilities.
Modern projects rarely need raw extrusions alone. Holes, slots, threads, and precision cuts transform profiles into assembly-ready components. Suppliers with integrated machining capabilities deliver finished parts rather than requiring you to coordinate secondary operations.
Key machining services to evaluate:
Integrated processing reduces transportation between subcontractors, prevents handling damage, and shortens lead times significantly. When exploring deep processing services, look for suppliers whose CNC capabilities match your precision requirements—particularly important for aluminum t rail applications or profiles requiring tight-tolerance hole patterns.
A supplier's QC system reflects their ability to maintain repeatable quality across production runs. According to industry evaluation criteria, key checks for procurement teams include:
Ask whether the factory provides process data for quality audits—capable suppliers track production parameters digitally and can demonstrate their quality systems upon request.
Professional manufacturers maintain certifications that validate their process control and traceability:
| Certification | What It Covers | Why It Matters |
|---|---|---|
| ISO 9001 | Quality Management System | Ensures documented processes and continuous improvement |
| EN 755-9 / EN 12020-2 | Dimensional Tolerance Standards | Confirms precision manufacturing capability |
| RoHS / REACH | Hazardous Substance Restrictions | Required for products entering EU markets |
| EN 1090-3 | Structural Aluminum Requirements | Essential for load-bearing European applications |
Lead time reliability often serves as the most practical indicator of supplier capability. According to industry benchmarks, typical timeframes include:
Ask how suppliers manage production scheduling during peak seasons. Factories operating ERP-based production systems generally deliver more consistently because they can visualize capacity constraints before they impact your delivery dates.
Strong technical communication differentiates professional manufacturers from simple traders reselling others' production. A capable extrusion partner will:
With over 30 years of industry experience, manufacturers like Shengxin Aluminium provide end-to-end technical support from die development through mass production—the kind of partnership that prevents problems rather than reacting after defects occur.
Evaluating aluminum extrusion suppliers requires looking beyond the price column. By analyzing die design capability, process control, machining integration, surface treatment options, and quality systems, you can identify partners that deliver consistent results, lower rework rates, and predictable timelines.
Consider creating a supplier scorecard covering:
The supplier relationship you establish now determines project success for years to come. With evaluation criteria clarified, you're ready to synthesize everything you've learned into a clear decision framework for your black aluminum extrusion project.
You've absorbed a tremendous amount of information—from anodizing chemistry to series numbering, T-slot mechanics to supplier evaluation. Now comes the moment to translate that knowledge into action. Whether you're building a sim racing rig, framing industrial equipment, or designing architectural elements, the decisions you make about black aluminum extrusion will determine project success for years to come.
The most critical consideration when selecting black aluminum extrusion is matching three elements simultaneously: finish type, series size, and supplier capabilities to your specific project requirements. Get any one of these wrong, and you'll face rework, delays, or compromised performance.
Let's distill everything into a clear decision framework. Think of this as your project planning checklist—the synthesis of technical specifications, practical considerations, and supplier criteria that guides you toward the right solution.
Your finish choice impacts durability, appearance, and long-term maintenance. Here's the simplified decision tree:
Match profile series to structural demands—oversizing slightly costs less than rebuilding an inadequate frame:
Remember that rectangular profiles like 3030 aluminum extrusion black or black aluminum h channel designs provide directional strength advantages when loads concentrate in specific orientations. Similarly, t extrusion and t aluminum profiles offer specialized connection options for door framing and panel integration applications.
Before requesting quotes or finalizing designs, ensure you've addressed these fundamental questions:
For complex custom projects, working with experienced manufacturers provides advantages that extend beyond unit pricing. Consider Shengxin Aluminium's comprehensive approach—their 30 years of industry experience, 35 extrusion presses spanning 600T to 5500T capacity, and integrated surface treatments including anodizing, powder coating, PVDF, and micro-arc oxidation for superior durability represent the kind of end-to-end capability that simplifies complex projects. Factory-direct pricing eliminates intermediary markups while ensuring quality accountability remains with a single manufacturing partner.
Ready to move forward? Follow this proven sequence to translate your requirements into successful procurement:
The investment you make in proper planning and supplier selection pays dividends throughout your project's lifecycle. Quality black aluminum extrusion from capable manufacturers delivers frames that look professional, perform reliably, and adapt to evolving requirements—whether you're building a single prototype or scaling to production volumes.
Complex custom projects benefit most from partnerships with experienced manufacturers who understand the interplay between profile design, finishing processes, and machining requirements. When your supplier handles everything from die development through mass production under one roof, you gain consistency, accountability, and the technical support that prevents problems before they impact your timeline. That's the difference between simply buying material and building a manufacturing relationship that supports your success project after project.
Black aluminum extrusion refers to aluminum profiles that have been treated with a black finish through anodizing or powder coating processes. During anodizing, an electrochemical reaction creates a porous aluminum oxide layer that absorbs black dye before being sealed, making the color integral to the metal. Powder coating applies dry pigmented powder electrostatically, which is then heat-cured to form a durable protective layer. Both methods transform standard mill-finish aluminum into sleek, corrosion-resistant profiles suitable for industrial machinery, consumer electronics, and architectural applications.
Series numbers correspond directly to profile cross-sectional dimensions in millimeters. A 2020 profile measures 20mm x 20mm, while a 4040 profile is 40mm x 40mm. These numbers also determine T-slot width and hardware compatibility—20 series profiles use 6mm T-slots with M5 hardware, 30 series accommodates M6 fasteners, and 40 series works with M8 hardware. Rectangular profiles like 20x40 provide directional strength advantages. Selecting the right series depends on load requirements, with heavier applications requiring larger profiles like 8020 for maximum structural integrity.
The choice depends on your priorities. Black anodized aluminum offers superior scratch resistance because the finish becomes integral to the metal surface—it cannot chip or peel. It excels in high-wear environments and provides excellent UV stability for outdoor use. Powder coating, however, offers greater color flexibility, thicker protective layers (2-4 mils vs 0.4-1 mil for anodizing), and better impact protection. For applications requiring maximum abrasion resistance, choose anodizing. For environments with impact risks or specific color matching needs, powder coating delivers excellent results.
Protecting the anodized or powder coated finish requires proper technique and tooling. Use miter saws with 80+ tooth carbide blades designed for non-ferrous metals, or band saws with 10+ teeth per inch. Apply cutting lubricant to reduce friction and heat that can crack the finish. Support workpieces properly to prevent vibration, and never let cut-off pieces fall freely. For drilling, use sharp carbide bits at slower speeds with light pressure. Consider ordering pre-cut lengths from manufacturers with CNC capabilities for precision work and guaranteed finish quality around cut edges.
Quality sourcing requires evaluating supplier capabilities beyond unit pricing. Look for manufacturers with appropriate press capacity (600T-5500T range covers most profiles), in-house die development, integrated surface treatment facilities, and CNC machining services. Suppliers like Shengxin Aluminium offer factory-direct pricing with comprehensive capabilities including anodizing, powder coating, PVDF, and micro-arc oxidation under one roof. Request samples to verify finish quality before production orders, and prioritize suppliers with ISO 9001 certification and documented quality control processes for consistent results.


 un service en ligne
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 français
 English
 Deutsch
 русский
 español
 português
 العربية
 ไทย
 Việt
 Українська